Home / 3D Printers
Best Multicolor 3D Printer
Top pick
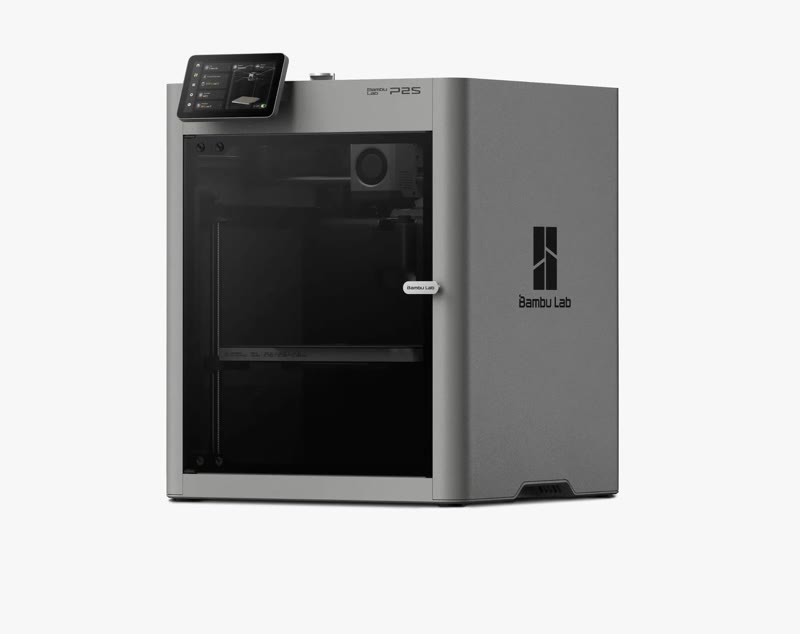
The P2S Combo is the best all-around choice for multicolor printing at home.
Budget and beginner choice Bambu Lab A1 Combo · Lower-Waste Two-Color Bambu Lab X2D Combo · High-temperature materials Bambu Lab H2D AMS Combo
| Printer | Best For | Price | Build Volume | Multicolor | Main Drawback |
|---|---|---|---|---|---|
1 |
Overall; home | About $699 | 256 × 256 × 256 mm | One nozzle, AMS 2 Pro; 4 loaded, expandable | Best remote features use Bambu’s cloud; local mode is available |
|
Bambu Lab P2S Combo details
| |||||
2 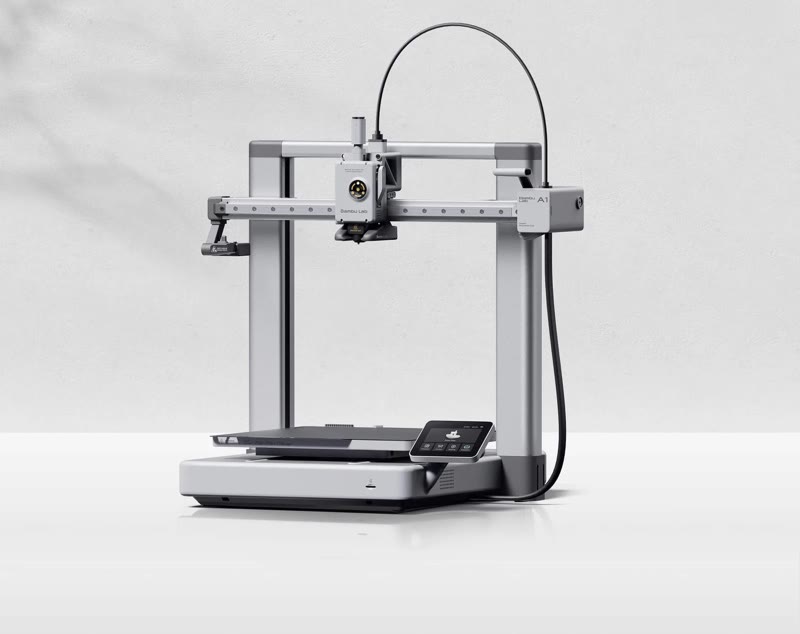 |
Budget; beginner | About $399 | 256 × 256 × 256 mm | One nozzle, AMS lite; 4 maximum | Open frame; limited to four colors |
|
Bambu Lab A1 Combo details
| |||||
3  |
Lower-waste two-color | $899 | 256 × 256 × 260 mm; 235.5 mm wide with both nozzles | Two switchable nozzles plus AMS 2 Pro; 4 loaded | Second nozzle is optimized more for support and accents than equal high-speed output |
|
Bambu Lab X2D Combo details
| |||||
4  |
Demanding material pairs | About $1,999 | 350 × 320 × 325 mm; 300 mm wide with both nozzles | Two direct nozzles plus AMS 2 Pro; 5 sources as bundled | Large, expensive and proprietary |
|
Bambu Lab H2D AMS Combo details
| |||||
4 printers shown
No matches. Remove a filter to see more options.
M manufacturer figure V measured result I reviewed ? unverified
Compare printers side by side
Choose two printers to compare their full details. Add a third if you need it.
Select two printers to start comparing.

Choose a multicolor printer by how often your models change color, not just how many spools it holds. Feeding several colors through one nozzle is affordable, but each change takes time and discards plastic.
Two nozzles reduce that waste for two-material jobs. Separate toolheads can save more time and material, but cost more to buy.
The Bambu Lab P2S Combo is my pick for most home users. It combines consistent printing, an enclosure, automatic setup and useful failure detection. Its four-spool AMS 2 Pro also dries compatible filament. The main drawback is plastic wasted as colors switch through the same nozzle.
If $699 is too much, the Bambu Lab A1 Combo is the sensible budget step down. For frequent two-color parts or mixed-material supports, spend more on the Bambu Lab X2D Combo.
Choose the A1 if an open printer and four colors meet your needs. Choose the P2S for everyday enclosed multicolor printing, or the X2D for frequent changes between two materials. The H2D is worth more only when you need its larger build area, extra heat and two capable nozzles.
Best Multicolor 3D Printer Overall: Bambu Lab P2S Combo
The P2S Combo is the strongest default because it gets the most important everyday things right before adding color. The enclosed CoreXY printer has a 256 × 256 × 256 mm build area, automatic bed and flow calibration, a hardened nozzle and extruder, a useful touchscreen and sensors for filament tangles, runout and power-loss recovery.
The included AMS 2 Pro holds four spools, actively dries many common materials up to 65°C and gives tool-free access to its filament tubes when something breaks inside.
That sounds like a specification list, but the reason it matters is recovery. A multicolor job can contain hundreds of swaps; one feed error can waste the hours already invested.
In an independent 300-hour P2S test, the printer paused on occasion for a filament or model issue but suffered no blockage or bed-release failure. The same review scored its print-quality test 28 out of 30 and found the surface finish excellent. One test period cannot establish a population-wide failure rate, but it is much stronger evidence than a quick unboxing.
The AMS 2 Pro keeps filament enclosed, measures humidity and can dry while the printer is idle without a separate power adapter. Bambu Studio maps colors and reports sliced filament use before you commit. Third-party filament works, although Bambu’s RFID spools fill settings automatically.

The main drawback is wasted filament. At each color change, the P2S cuts and pulls back the old filament, loads the next one, then pushes out the mixed plastic and wipes the nozzle.
A model with small color details on many layers can produce more waste than usable print. One reviewer reported large piles of this waste during testing. Drying and faster feeding make the printer easier to use, but they do not remove the waste from sharing one nozzle.
You should also understand the material limit. Bambu’s AMS 2 Pro specification excludes generic TPU and TPE, damp PVA or BVOH, PET-CF, TPU 95A and other carbon- or glass-filled filaments outside the named supported range. Such filament may print from an external spool, but it cannot automatically participate in the same feeder-controlled job.
Spools must also fit roughly 50–68 mm wide and 197–202 mm in diameter, so odd reels may need respooling.
Don’t buy the P2S if low waste is your first requirement or if you regularly pair flexible filament with rigid plastic in one part.
The closest alternative is the X2D Combo. It costs about $200 more and its second Bowden-fed nozzle is slower, but it can keep two materials in separate melt paths. That makes the X2D better for two-color models, easy-release support interfaces and selected rigid-plus-flexible parts. For ordinary four-color PLA, the P2S is simpler, cheaper and backed by the longer high-hour test.
Best Budget Multicolor 3D Printer: Bambu Lab A1 Combo
At about $399 with the AMS lite, the A1 Combo is the cheapest complete setup I’d comfortably recommend. The printer’s 256 mm cube build area matches the P2S, and its automatic bed leveling, vibration compensation and flow calibration remove several chores that used to make inexpensive printers frustrating.
The four-spool AMS lite handles loading and color selection, while separate short Bowden tubes make broken filament easier to reach than in a long shared path.
Anycubic lists a cheaper option: the Kobra 3 V2 Combo with ACE Pro at $355. Its enclosed feeder also dries filament, which looks useful on paper.
But an independent four-month test found the multicolor function frustrating, even though basic print quality stayed good. For a guide focused on multicolor printing, that matters. The $44 saving is too small for me to recommend it over the better-tested A1 system.
The A1’s low price still buys compromises. It is open, so drafts affect temperature-sensitive materials and fumes aren’t contained. AMS lite does not dry its four exposed spools.
Bambu’s current quick-start guide says not to feed TPU, TPE, absorbent PVA or third-party fiber-reinforced filaments through it. You can print compatible flexible filament from the external holder, but not as an automatic AMS color in the same ordinary workflow. One AMS lite is the ceiling, so four loaded colors cannot be expanded.
Allow for extra printing time and wasted filament, too. One test printed a Flexi Factory panda on the A1 in 2 hours 40 minutes using one color. Three colors took 6 hours 46 minutes, about 154% longer.
The report did not include enough weight data to compare material costs. Even so, it shows why the purchase price is only part of the cost.

If you already own an A1, compare the add-on price with the combo discount before buying an AMS lite separately; bundles are often cheaper. An unofficial feeder conversion is not the budget answer for supported operation.
Choose the A1 Mini Combo only when its 180 mm build cube definitely fits your work; otherwise the full-size A1 prevents an early replacement.
The closest alternative is the P2S Combo. Spend the extra money when you need an enclosure, integrated drying, harder-wearing filament-path parts or expansion beyond four colors. For PLA signs, toys, organizers and display pieces, the A1 preserves most of the useful automation at much lower cost.
Best Multicolor 3D Printer For Beginners: Bambu Lab A1 Combo
A multicolor machine can be a first printer, but it adds more places for feeding problems to occur.
The A1 Combo is an easy starting point. It calibrates itself, has a clear touchscreen and uses a clip-in hotend. The AMS lite’s exposed spools and short tubes also make broken filament easier to find and remove.
Reviewed A1 tests found useful Bambu Studio presets, practical model-coloring tools and easier jam access than the original AMS. Files can arrive through Bambu’s cloud, a local network or microSD. Bambu Studio runs on Windows, macOS and Linux; the phone app is optional.
What a new owner will notice first is not poor print quality but housekeeping. Every change creates a small purge piece behind the machine, so you need a bin or chute with clear space. Four exposed rolls take more desk area than the printer alone and can absorb moisture.
You must learn to read the slicer’s time and filament estimates before pressing print. A model painted with tiny dots on hundreds of layers can be dramatically slower and more wasteful than one divided into broad color regions.
The second compromise is material handling. The A1 itself can print TPU from an external spool, but AMS lite cannot automatically feed ordinary TPU.
An enclosure is also absent, so this is mainly a PLA and PETG recommendation. A beginner who expects ABS, nylon or composites should not buy it merely because the nozzle temperature looks sufficient; stable chamber conditions and feeder compatibility matter more than the maximum number on the heater.

The A1’s 2024 heatbed-cable recall deserves context. Current units use a redesigned cable with Kevlar reinforcement, thicker insulation and a longer strain relief. Check that a used machine received the recall remedy; its serial and cable condition still matter.
Choose the P2S Combo if you already know you need enclosed ABS or ASA printing, tidier filament storage or more than four loaded colors later. The A1 costs less and makes its moving and feeding parts easier to reach.
If open firmware and full offline control are priorities, compare Prusa’s systems, though its supported multicolor setups cost more.
Best Multicolor 3D Printer For Home Use: Bambu Lab P2S Combo
For home use, I’d return to the P2S Combo. Its enclosure keeps moving parts behind a door, contains stray purge inside a predictable rear outlet and stabilizes the print environment.
The printer body occupies about a 15-inch-square patch, although the AMS on top, rear purge clearance and door swing mean the real occupied space is larger. Measure the shelf in three dimensions and leave access to the back; the nominal machine footprint is not the installation footprint.
The P2S also reduces filament-storage clutter. Its AMS 2 Pro holds four spools in a sealed enclosure, reports humidity and rotates rolls during drying. Bambu says nylon, PC and several other filaments need higher temperatures than its 65°C maximum; for those, it recommends the hotter AMS HT.
An enclosure is not a ventilation permit. ABS, ASA and some engineering materials can emit particles and volatile compounds; filtration reduces exposure but does not make an occupied bedroom an appropriate workshop. Put the machine in a ventilated utility space for those materials.
PLA printing is the more comfortable shared-room use case. The P2S has active motor-noise control, yet fans, rapid movement, retraction and repeated feeder changes remain audible. Don’t place it beside a bed or a video-call microphone.
Bambu makes remote monitoring convenient, but its fullest remote features use the company’s service. Standard LAN mode through Bambu Connect requires neither internet access nor an account.
Optional developer mode allows more third-party control and leaves network security to the owner. USB and local use reduce cloud dependence, but Prusa provides more open access to its software and hardware.
The closest alternative is the A1 Combo. It is quieter in its slow mode and cheaper, but its open AMS rack spreads four spools across the room, offers no drying and leaves the moving bed exposed.
Choose it for a dedicated craft table and PLA. Choose the P2S for a smaller, cleaner installation—unless purge pieces dropping behind the printer, cloud-centered convenience or fan noise are unacceptable.

Best Multicolor 3D Printer For Lower-Waste Color Changes: Bambu Lab X2D Combo
The X2D Combo is the best evidenced lower-waste choice for jobs dominated by two colors or two materials. It keeps one direct-drive main nozzle and one mechanically selected, Bowden-fed auxiliary nozzle in the same tool assembly.
Because each hotend retains its material, switching between them does not require flushing one color out of a shared melt zone. A small prime tower is still normally needed to stabilize pressure, so “dual nozzle” does not mean zero waste.
The cleanest measurement comes from an independent same-machine test. A 12 g multicolor Benchy using standard settings produced about 20 g of waste and took 2.7 hours with both X2D nozzles. Routing the same colors through one nozzle produced about 70 g of waste—52 g of it flushing—and took 5.8 hours.
Removing the prime tower shortened the dual-nozzle slice to 1.7 hours but visibly harmed quality, so that is not a fair operating recommendation.
Another test printed 15 black-and-white miniatures in 13 hours 54 minutes. It used 11.5 g in the nozzle-preparation tower. The reviewer calculated a saving of 101 g compared with passing both colors through one nozzle. Close-up photos showed slightly rougher detail from the right nozzle.
The X2D has two nozzles, not four independent tools. Its AMS 2 Pro holds four spools, but extra colors assigned to one nozzle still need loading, unloading and flushing.
The Bowden-fed secondary nozzle is slower than the main direct-drive nozzle. In one simple cube test, it took roughly twice as long. Bambu mainly recommends it for the material where supports touch the model.
At $899, the X2D costs about $200 more than the P2S Combo. In one Benchy test, its two nozzles saved 50 g of filament per print. At an assumed $25 per kilogram, that saves $1.25 each time. You would need roughly 160 similar prints to recover the extra $200 through filament savings alone.
Faster printing and cleaner color boundaries may also be valuable, especially for repeat orders. Occasional users are unlikely to recover the extra cost quickly.
The established five-tool Prusa XL wastes even less filament when printing with three to five materials. Its replacement, the XL+, had only just started reaching reviewers at launch. I would wait for current independent tests before recommending that a home user spend about $4,000 on it.
Choose the X2D for frequent two-material printing or the P2S for everyday four-color models. For low-waste printing with four or five colors, wait for tests of the new tool-changing machines.
Best Multicolor 3D Printer For Demanding Material Combinations: Bambu Lab H2D AMS Combo
The H2D AMS Combo is the specialist choice when “multicolor” really means different physical properties. Its two separately heated direct nozzles can keep a model material and support material apart, or alternate a rigid polymer with a flexible one without repeatedly flushing a shared hotend.
The enclosed machine adds an actively managed chamber, hardened filament-path components and a larger dual-nozzle work area of 300 × 320 × 325 mm.

This matters for combinations such as PLA with PETG as a breakaway interface, a structural polymer with PVA or BVOH soluble support, or selected rigid and flexible sections. Separate melt paths reduce color contamination and avoid asking two materials with different transition behavior to share one nozzle.
In independent H2D testing, long support-material prints remained consistent, and a TPU 90A shoe ran for roughly 70–80 hours per pair. Another reviewer also found automatic dual-nozzle alignment effective and loading through AMS 2 Pro straightforward.
Do not translate that into “any two filaments work together.” Materials still need compatible print temperatures, shrinkage behavior and adhesion at their interface. A flexible insert can mechanically interlock with a rigid shell even when the polymers do not bond well; a flat bonded joint may peel.
Soluble supports must be dry and need safe disposal. Abrasive composites require a suitable hardened nozzle. High-temperature materials need the chamber profile specified for that filament, not merely a hot nozzle.
The AMS 2 Pro accepts many common filaments and specified Bambu composites, but excludes ordinary TPU, TPE and some rough or oversized filaments. One reviewer fed TPU from a separate dry box and found the routing awkward. Some nozzle and firmware setups require disconnecting the AMS path.
Current dual-nozzle jobs also require matching nozzle sizes and types, so two hotends do not let you mix a 0.4 mm detail nozzle with a 0.6 mm support nozzle.
The price is decisive. An authorized US retailer listed the H2D AMS Combo in stock at $1,999 on September 4, 2026. It weighs about 31 kg, takes around 45 minutes for its initial self-check and uses proprietary replacement parts. Avoid it if color is mostly decorative PLA.
The X2D is the closest alternative. It has two nozzles, a 65°C chamber and hardened nozzles for $899. Its auxiliary Bowden-fed nozzle is slower than the main nozzle. Even so, a 250-hour test successfully combined Bambu AMS-compatible TPU with PLA and printed several engineering materials.
Choose the X2D for support materials and occasional parts that mix flexible and rigid plastic. The H2D is worth more when you regularly need larger parts or two direct-drive nozzles working at full speed.
What Color Changes Add To Print Time, Waste And Failure Risk
A single-nozzle color change has five basic stages: cut the current filament, retract it, feed the next spool, purge until the old color leaves the melt zone, then wipe and re-prime the nozzle. The machine pauses model deposition throughout most of that sequence.
More colors do not automatically cause more waste; the number of changes across layers is what matters. A four-color sign with four large vertical regions may be punishing, while a four-color object divided by height may need only three changes.
That difference matters most on small detailed objects, where the purge required for each swap is large beside the plastic deposited in the model, and least on big objects with broad, uninterrupted color regions.
No public test gives a fair, shared low-change and change-heavy file across all four finalists with every setting and measured output disclosed. Mixing unrelated numbers would create a false ranking. The narrower evidence below changes one architecture or color plan while holding the machine and model constant.
A Change-Heavy Measured Example
An independently tested X2D Multicolor-3D-Benchy is the most complete reproducible slice available among the finalists. With standard settings and the same 12 g model, using two nozzles took 2.7 hours and made about 20 g of prime-tower waste.
Forcing both colors through one nozzle took 5.8 hours and made about 70 g of waste, including 52 g attributed to flushing.
That gives a model-to-waste ratio of roughly 1:1.7 with two nozzles and 1:5.8 with one. At a simple September 2026 filament assumption of $25/kg, the model plastic costs $0.30. Total plastic becomes about $0.80 in dual-nozzle mode and $2.05 in single-nozzle mode.
Electricity, failed prints, taxes and spool remnants are excluded. The point is not that every Benchy costs those amounts; it is that frequent changes can make transition plastic dominate a small model.
The same test showed why disabling the prime tower is not free optimization. It cut estimated dual-nozzle time from 2.7 to 1.7 hours, but the tester reported a major quality decline.
Purge and prime volumes are conservative partly because clean color boundaries and stable extrusion need a margin. Reducing them requires validation with your exact light-to-dark transitions and material.
A Lower-Information, Lower-Change Comparison
One reviewer printed the same Flexi Factory panda on the A1 in one color and three colors. The one-color version took 2 hours 40 minutes; three colors took 6 hours 46 minutes, an increase of 4 hours 6 minutes, or about 154%.
The report omitted mass and material cost, so it cannot support a waste ratio. It does show why the slicer preview should govern each print decision.
For another two-nozzle data point, one test I reviewed used 15 black-and-white X2D miniatures. The job used 11.5 g in the prime tower and saved a calculated 101 g over one-nozzle routing. The model mass and one-nozzle time were not reported, so again it belongs as supporting evidence, not a complete cross-machine score.
Where Changes Fail
Most failures occur in the path, transition or restart. A spool can bind because its rim or diameter does not suit the feeder. Brittle damp filament can snap inside a tube. Soft TPU can buckle when a feeder pushes it. A cutter can wear, a retracted tip can form a bulb that catches, or fine debris can reduce traction.
At the nozzle, too little purge leaves color contamination; too much consumes time and plastic. A parked or idle nozzle can ooze, making a prime tower necessary even without color mixing.

Recovery quality matters because a pause is not always a rescue. Good runout and tangle detection can stop before grinding, while accessible tubes let you clear the path without losing alignment. But no sensor can recover a model already knocked loose, and resuming after a long thermal pause may leave a visible seam or weak layer.
Keep filament dry, use supported spool sizes, inspect cutters and PTFE tubes, and place the purge outlet where waste cannot back up into the mechanism.
Check the slicer’s separate estimates for the model, supports, flushed plastic and preparation tower. If color changes waste more material than the model uses, try larger blocks of color or several copies in one job.
You can also flush into hidden infill where color mixing will not show, or print colored pieces separately. These changes can save more than a higher advertised printer speed.
Choose A Multicolor System By Its Deal-Breakers
Start with the job, not the brand. If you want four-color PLA decorations with minimal setup, a single-nozzle feeder is the economical answer.
If two colors or model-and-support materials switch on nearly every layer, two nozzles justify their premium. If three to five distinct materials must remain in separate hotends, a toolchanger is the clean architecture—but current replacement models need independent validation before they deserve a recommendation.
Material compatibility can eliminate a machine immediately. “Multi-material” describes multiple feedstocks, not guaranteed compatibility. A feeder supporting PLA and TPU separately does not prove it can switch between both automatically, nor that the two polymers will bond.
For ordinary A1 AMS lite use, TPU, TPE and damp soluble supports are explicit exclusions. AMS 2 Pro accepts Bambu’s specially formulated “TPU for AMS,” but not generic TPU. If your design needs soft 90A material, plan an external dry route and verify the nozzle assignment before buying.
Drying is also different from storage. A sealed feeder slows moisture uptake; it does not necessarily restore wet nylon.
AMS 2 Pro reaches 65°C and Bambu itself points owners of higher-temperature materials toward the 85°C AMS HT. AMS lite supplies neither heat nor a sealed box. Add the price and shelf space of a dryer when comparing an A1 with an enclosed combo.
Software is the next hard fork. Bambu Studio provides the most integrated painting, spool mapping and estimate workflow here. It supports Windows, macOS and Linux, and local printing does not require an internet account under Bambu’s stated LAN policy.
Yet Bambu controls the authorization layer and the best phone monitoring runs through its service. Developer mode restores broader third-party access but shifts network-security responsibility to you.

Prusa remains a strong choice for offline use. Its documentation says you can slice models, transfer files and update firmware without an internet connection. PrusaLink adds control through a local browser.
At launch, however, XL+ review units were only just going out, and the planned 60°C enclosure heater was not shipping. Those limits keep it out of the top picks for now.
Finally, distinguish multicolor from full color. These printers place a few discrete filament colors. They do not reproduce photographic continuous color like industrial binder-jet systems. Slicer “painting” assigns regions, faces or layers to loaded spools; it cannot create a color that is not loaded, except through experimental visual blending that may show bands.
If you want minimal manual swapping, buy the complete feeder bundle. If you want minimum purge across many colors, wait for a tested multi-tool system rather than assuming a 16- or 24-spool claim solves waste.
Is A Multicolor 3D Printer Worth It?
Yes, when color is part of the function or you use it often enough to justify the cleanup. Labels printed into tool drawers remain readable after scratches. Color-coded classroom parts, wiring guides and controls communicate without paint. Display models, toys and signs can come off the bed finished.
Automatic spool backup can also continue a long single-color job from a second matching roll, a benefit unrelated to decoration.
The case weakens for occasional accents. If a logo appears on only the top few layers, a pause and manual filament change may deliver the same result with almost no hardware cost.
If a model divides cleanly into parts, printing colors separately and assembling them avoids purge and often finishes faster. Paint, decals or markers make more sense when you want shading rather than hard color regions.
A purpose-built combo is usually cheaper and less troublesome than adding the feeder later. An upgrade makes sense when you already own a specifically supported printer and the standalone accessory, cables, hub and power supply cost less than replacing it.
Unofficial conversions can be rewarding projects, but they are not equivalent to a supported consumer setup with tested slicer profiles and warranty coverage.
I would actively steer a PLA-only hobbyist who prints one decorative multicolor object every few months away from the H2D. Its $1,999 package, large footprint and dual-material complexity solve problems that person does not have.
I would also steer a renter in a bedroom away from treating any enclosure as permission to print ABS beside the bed.
For frequent four-color display work, the P2S Combo is worth it if you accept purge. For a first printer or tight budget, the A1 Combo reaches the same basic result. For repeated two-color pieces or soluble-support interfaces, the X2D’s savings are tangible. Otherwise, buy a strong single-color printer.

Multicolor 3D Printer FAQ
Can Resin 3D Printers Print In Multiple Colors?
Not in the automated consumer sense covered here. A typical desktop resin printer cures one vat of resin, so it makes one material and color per job. You can pause, clean carefully and change resin, but contamination, handling and layer adhesion make that a manual technique rather than a feeder system.
Industrial full-color machines use different processes and prices. For consumer resin detail, painting the cured model is normally the practical route.
How Many Colors Can A Multicolor Printer Use In One Job?
Loaded capacity and expansion claims are different. A1 and AMS lite hold four and cannot add a second AMS lite. The P2S, X2D and H2D combos reviewed here include one four-slot AMS 2 Pro; compatible hubs and extra AMS units can raise the number of available spools, but every extra color may add switching time, purge and hardware cost.
Dual-nozzle machines keep only two materials in separate hotends. More loaded spools do not mean more simultaneous extrusion.
Can Different Filament Materials Be Combined In One Print?
Sometimes. The feeder must physically handle each filament, the nozzle and chamber must reach appropriate temperatures, the materials must tolerate the same bed environment, and their interface must bond or interlock as the design requires.
PLA and PETG can be useful precisely because they separate as support interfaces. Generic TPU often cannot pass through automatic feeders. Check the manufacturer’s exact filament table and test a small joint before committing to a long part.
What Files Or Slicer Work Does A Multicolor Print Require?
You can import a single STL or 3MF and paint regions in the slicer, or import a multi-part 3MF/CAD assembly whose bodies already represent colors. Then map each region to a feeder slot or nozzle. Use the manufacturer profile first, inspect the purge and prime-tower preview, confirm every spool assignment and save the project as 3MF so those mappings remain.
Plain STL does not store color. A prepared G-code file should only run on the exact printer, nozzle and material setup for which it was sliced.
The Multicolor Printer To Choose
Buy the Bambu Lab P2S Combo if you want the safest general recommendation. It combines an enclosed, well-tested printer with four-color automation, active filament drying, helpful sensors and a slicer that shows the cost of a job before you start. Its weakness is substantial single-nozzle purge, not a minor footnote.
Choose the A1 Combo for a lower-cost setup using mostly PLA and PETG. Choose the X2D Combo for frequent changes between two colors or separate support material; tests show that the second nozzle can save time and plastic. Move to the H2D when large, repeated two-material jobs justify its extra cost.
Do not buy any multicolor system merely to avoid painting one occasional model. If the slicer predicts more transition plastic than finished part, redesign, batch copies, split the model or use a manual change.
The right printer is the one whose waste, material path and recovery routine you will accept after the novelty of four loaded colors wears off.


