Flashforge Adventurer 5M Pro Review
Costs more than the open Adventurer 5M
Our verdict
I’d choose the Adventurer 5M Pro for single-color hobby projects and small batches when I’ll use its ready-built enclosure. Quick-change nozzles make it easier to switch between detailed models and simpler parts; for mostly PLA and PETG, I’d lean toward the less expensive Adventurer 5M.

Best atSingle-color everyday projects with an enclosure ready for trying ABS and ASA.
Less suited toAutomatic multicolor printing, oversized parts and a beginner’s focus on flexible TPU.
The Key Specs
| Print area | 220 × 220 × 220 mmAllow space for supports and borders; larger projects need splitting into sections. |
|---|---|
| Enclosure | No dedicated chamber heaterRetains bed heat for ABS and ASA, but material settings and ventilation still matter. |
| Nozzle choices | 0.4 mm installed; spare 0.6 mm includedStart with 0.4 mm for general work; 0.6 mm suits thicker layers when fine detail matters less. |
| Material fit | Start with PLA or PETGFlexible TPU takes more patience; carbon-fiber-filled PLA/PETG needs the specified wear-resistant 0.6 or 0.8 mm assembly. |
| Color printing | Single color; no compatible AD5X switching moduleAutomatic four-color printing requires the separate AD5X. |
Which Version Should You Buy?
- Adventurer 5M Pro
- Choose it for the complete enclosure, filtered circulation, extra cooling fan, camera and interior lighting.
- Adventurer 5M
- Costs less for mostly PLA/PETG and keeps the same print area, automatic leveling and quick-change nozzle options; an optional enclosure kit does not add all the Pro’s hardware.
Budget beyond the printer. Allow for filament, plate glue, replacement filters, guide lubrication and suitable ventilation. A spare nozzle assembly can reduce downtime; replacing the combined nozzle and heater costs more than a simple screw-in tip. Moisture-sensitive filament may also need drying equipment.
Also consider: Flashforge AD5X. Choose its four-color system if automatic color changes matter; its 220 mm cube gives no extra space for larger parts.
More Specs And Ownership Details
| Setup | Mostly assembled, with automatic leveling and vibration calibration; watch the first layer and prepare the plate. |
|---|---|
| Temperatures | Nozzle up to 280°C. Bed documentation lists both 100°C and 110°C; confirm the limit with Flashforge before buying for filament requiring more than 100°C. |
| File transfer | USB, Wi-Fi or Ethernet; local-network printing is available. |
| Placement | Body roughly 15 × 16 × 18 inches, excluding the spool holder. Leave room behind, above and in front for loading and access. |
| Filtration and upkeep | HEPA and activated carbon do not replace ventilation. Clean the plate and chamber, lubricate guides and replace filters according to the manual. |
| Nozzle changes | Follow the manual’s cooling and power-off instructions, then level again after a swap; deeper feed-path jams can require disassembly. |
I’d consider the Flashforge Adventurer 5M Pro if you want a mostly assembled printer for everyday projects, with an enclosure that also lets you try plastics such as ABS and ASA. Its quick-change nozzles are useful when you switch between detailed models and larger, simpler parts.
The main catch is paying extra for features your prints may not need. For ordinary PLA and PETG, the cheaper Adventurer 5M deserves the first look. You’ll also need to choose compatible software and find a spot with enough ventilation where the fan noise won’t bother you. I’d choose the Pro for single-color hobby projects and small batches if you’ll actually use the enclosure.
Getting The 5M Pro Ready For Your First Print
Setup is manageable for a beginner. Remove the packaging and four screws securing the print bed, the platform you print on. Then attach the rear spool holder and follow the touchscreen prompts. You don’t have to build the frame or wire the moving parts.
The standard package includes filament—the plastic fed into the printer—plus glue, tools, a USB drive and a spare 0.6 mm nozzle. The installed nozzle is 0.4 mm; these sizes describe the opening the melted plastic passes through.
Initial calibration checks the bed and compensates for vibration. Automatic leveling sets the gap between the nozzle and printing surface, saving you a manual adjustment. Still, watch the first layer: plastic should stick to the plate instead of being dragged around. If it doesn’t, stop and address the problem before wasting more filament.
For the first print, feed PLA—the usual beginner plastic—through the sensor and guide tube, then use the loading menu. Confirm that plastic comes out of the nozzle. Flashforge’s startup instructions also call for glue on the plate; automatic leveling doesn’t replace bed preparation.
Once the print has cooled, remove and gently flex the steel plate to release it. Keep the coated printing surface clean, and recalibrate after changing the nozzle or plate.
The build space is 220 × 220 × 220 mm, about 8.7 inches in each direction. Phone stands, small organizers and brackets are realistic projects. Allow room for any printed supports that hold up overhanging parts, or an extra border that helps the print stick. If your project is too big to fit, you’ll need to print smaller sections and put them together.
How The 5M Pro Balances Speed And Print Quality
The 5M Pro can finish useful prints quickly, but the advertised 600 mm/s isn’t the speed of an entire job. Flashforge’s technical guide identifies that as maximum travel speed: movement between printing locations. Corners, cooling pauses and how quickly the nozzle can melt plastic all affect completion time.
A larger nozzle can shorten printing time if you’re willing to accept less detail. The slicer software turns your model into layer-by-layer instructions for the printer.
In one reported test, a frog model enlarged to 250% of its original size took 6 hours 52 minutes with a 0.4 mm nozzle and OrcaSlicer’s default settings for 0.2 mm layers. A 0.6 mm nozzle with 0.3 mm layers finished the same model in just over four hours, with more visible steps on curved surfaces. Both nozzle size and layer height changed, so this wasn’t a nozzle-only speed test.
A reported PETG wall hook finished in 1 hour 37 minutes with a 0.6 mm nozzle and a good surface finish. That test used Orca-Flashforge 1.0.2 and firmware 2.7.2, the software running on the printer itself. The report didn’t specify the hook’s layer height or test it under weight, so it doesn’t establish how much weight your hook will hold.
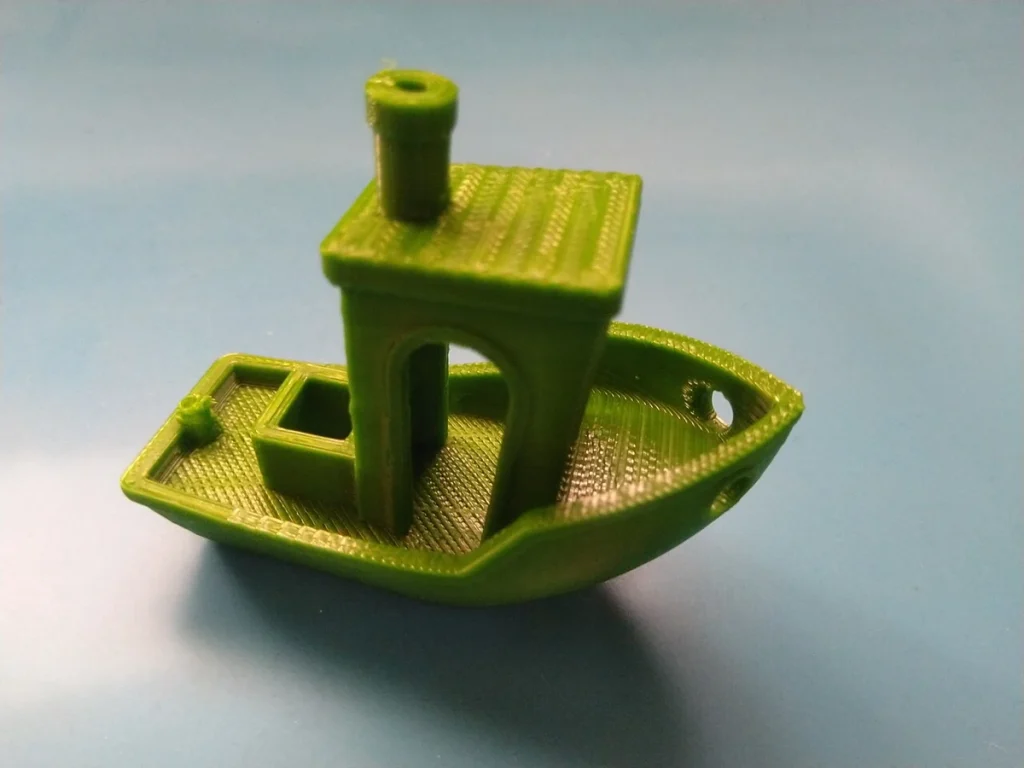
Surfaces printed without support underneath can be less predictable. These include overhangs, where a layer extends beyond the one below it, and bridges across open gaps.
One reported Mini All-in-One test finished in 58 minutes with good overhangs and bridges but heavy stringing—fine plastic threads between features. Another early test using standard print settings found clean outer surfaces but poor undersides. The models and settings differed, so these results don’t tell you exactly which unsupported shapes will print cleanly.
Start with the 0.4 mm nozzle for general work. Use 0.6 mm when thicker layers and less fine detail are acceptable. If a lid has to fit a box or a bracket needs bolt holes, print one example and check it before filling the bed with copies. A fast, attractive sample doesn’t guarantee that every part will fit your hardware without adjustment.
Which Materials Make Sense In The 5M Pro
PLA and PETG are the sensible starting points. PLA suits decorative pieces and many indoor projects; PETG is worth considering for tougher everyday parts. Use the profile for your material, meaning the saved combination of temperatures, cooling and printing settings. Settings that work for PLA won’t necessarily suit another plastic.
ABS and ASA make better use of the enclosure because they can shrink as they cool, causing parts to lift or crack. The chamber retains heat from the bed to reduce this risk; it has no dedicated chamber heater.
Flashforge specifies internal air circulation for ABS/ASA, which recirculates chamber air to retain warmth. External circulation, specified for PLA/PETG, exchanges air with the room to help cool the chamber. It isn’t an exhaust connection to outdoors, and neither mode makes every large ABS part straightforward.
An ASA test shows what’s possible: an open framework, or lattice, filling the build space printed in 24 hours 44 minutes with no reported warping. It used 100% infill, meaning the bars forming the lattice were filled with plastic rather than partly hollow. That open shape matters: the result doesn’t show how a solid box with a broad, flat base would print, or whether you could reliably print a whole batch.
The nozzle reaches 280°C. Bed-temperature documentation conflicts: the US product page lists 100°C, while the quick-start guide lists 110°C. If your filament needs a bed hotter than 100°C, ask Flashforge to confirm the limit for the printer you’re buying before choosing it for that material.
TPU, the flexible plastic used for grips and soft parts, takes more patience. Flashforge’s printer guidance favors 0.6 or 0.8 mm nozzles for TPU, although its newer filament guide also permits 0.4 mm for Flashforge TPU-95A and TPU-64D.
TPU absorbs moisture, which can turn to steam in the hot nozzle. The resulting bubbles can disrupt plastic flow and leave rough surfaces or weak bonds between layers. Follow your filament maker’s drying instructions to remove moisture before printing, use settings for that exact filament, and start with a small print.
In one reported test, TPU printed through a 0.4 mm nozzle but had defects, and the printer jammed when changing filament afterward. Another test needed slow 30–40 mm/s printing. Neither test establishes moisture as the cause of its problems or shows that drying would prevent them. I wouldn’t make this my first choice for a beginner mainly interested in flexible parts.
Carbon-fiber-filled PLA or PETG can wear down a nozzle. Use the wear-resistant 0.6 or 0.8 mm nozzle assembly specified for these materials; the standard 0.4 mm stainless-steel nozzle isn’t that option. Compatibility with those materials doesn’t mean every nylon or engineering plastic will work. Check the exact filament’s drying instructions, nozzle requirements and required nozzle, bed and chamber temperatures.
Sending Files And Checking Prints On The 5M Pro
Flashforge now recommends Flash Studio Desktop as its slicer. Older instructions may call it Orca-Flashforge. Its phone app for checking and managing prints is Flash Studio Mobile, formerly Flash Maker.
FlashPrint 5 and standard OrcaSlicer also remain listed in the printer’s downloads. Whichever slicer you choose, select the saved settings for the 5M Pro, called a printer profile, and the installed nozzle size. Standard OrcaSlicer and Flashforge’s own version are separate programs; a connection tutorial for one may not apply to the other.
You can transfer files by USB, Wi-Fi or Ethernet. Flash Studio Desktop supports cloud transfer and LAN Only mode, which keeps the connection on your local network.
Mobile requires an internet connection and a printer linked to your account; it doesn’t work in LAN Only mode. Flashforge currently specifies firmware 5.1.7-2.2.3 or later for Mobile on the 5M Pro. Check that your printer’s firmware meets the app’s requirements during setup.
Early reported tests found inconsistent leveling and limited FlashPrint profiles. Flashforge’s June 2024 firmware 2.7.1 notes describe a fix for leveling failing to run even when the option was selected. By August 2024, reported testing with Orca-Flashforge 1.0.2 and firmware 2.7.2 successfully sent prints over Wi-Fi. That successful transfer doesn’t prove every connection problem has disappeared, but older reports of failed transfers don’t describe every software version or setup.
Treat the built-in camera as a convenient way to check progress. It doesn’t replace looking closely at the first layer or inspecting a finished part. USB also remains useful when you want to print without sorting out a network connection. For small batches, choose a transfer method you can use consistently; you don’t need to try every app.
Finding Room For The 5M Pro And Keeping It Running
Leave room around the printer so you can use it comfortably. The body is roughly 15 inches wide, 16 inches deep and 18 inches tall, excluding the spool holder. You need access behind it to change filament, room to open the front door and clearance above the hinged lid. A tight shelf that fits the printer’s outline may be awkward to use.
I’d put it on a sturdy bench away from where you sit for hours. The enclosure reduces some sound, but the cooling and circulation fans remain audible. A low-noise mode is available.
Flashforge advertises 50/55 decibels (dB), while one test reported a 68 dB average. Without matching measurement conditions, those numbers aren’t directly comparable. They can’t tell you how loud it will sound beside your desk, and “enclosed” doesn’t mean quiet enough for bedroom printing.
The HEPA and activated-carbon filters are useful, but their presence doesn’t prove the air in your room is safe. Trapping particles and removing gases are different tasks. Don’t treat the advertised removal percentage as proof that emissions can’t escape.
Use a well-ventilated location away from where people sit; for frequent ABS or ASA work, plan suitable exhaust near the printer that carries emissions outdoors. The enclosure doesn’t replace ventilation.
You’ll need to clean the plate and chamber, lubricate the guides that moving parts travel along, and replace filters. Follow the manual’s lubrication schedule. Flashforge recommends replacing the filters every 300 printing hours, or sooner when visibly dark. That schedule doesn’t guarantee the filters will stay effective for all 300 hours.
Nozzle swaps are convenient because the assembly releases with clips. Follow the manual’s instructions for cooling and turning off the printer before changing the nozzle, then run leveling again after the swap.
Clearing a jam farther up in the filament-feeding mechanism can require disassembly, so the quick nozzle release doesn’t make every blockage a quick fix. Short reported tests also can’t tell you how many years the printer will last.
When The 5M Pro Is Worth The Extra Cost
For mostly PLA toys, desk organizers and PETG brackets, I’d lean toward the regular Adventurer 5M. It costs less and has the same 220 mm cube of printing space, automatic leveling and quick-change nozzle options.
The Pro adds a complete enclosure, filtered air circulation, an extra cooling fan, a camera and lighting inside. Those extras make more sense if you expect to print ABS/ASA or want the enclosed setup ready from the start.
The extra fan can help newly laid plastic harden before an unsupported overhang sags. Too much cooling can make materials such as ABS and ASA lift or crack, so use cooling settings suited to the plastic. The mixed overhang results mean you may still need to adjust those settings to get clean undersides.
You can buy an enclosure kit for the regular 5M if you’re happy to install it yourself, but panels alone don’t reproduce all the Pro’s filtration, cooling and monitoring hardware. If you already know you want those features, compare the complete setups rather than assuming the cheapest base printer will be the best choice after upgrades.
Both 5M models use the same replacement nozzle assemblies. You replace the nozzle and its heating assembly together, which costs more than replacing a simple screw-in tip. Choosing the regular 5M doesn’t avoid that expense. Budget for filters on the Pro, and consider a spare nozzle if a delayed batch would be inconvenient.
Flashforge’s limited warranty is 12 months for the printer, with a shorter three-month term for the extruder, which feeds filament into the nozzle. Check the seller’s service terms too.
If you want automatic multicolor printing, look at the separately sold AD5X with its four-color system. Its filament-switching module isn’t compatible with the 5M Pro. The AD5X also prints within a 220 mm cube, so you won’t gain room for bigger parts.
The Pro is worth the extra cost when you’ll use its enclosure and cooling and are willing to learn material settings and routine maintenance. For parts larger than its 220 mm cube, choose a bigger printer or plan to assemble smaller printed sections.


