Formlabs Form 4 Review
Premium · substantially more than typical consumer resin printers
Our verdict
I’d choose the Form 4 for frequent detailed prototypes and small batches once a sample of my intended part passes inspection. Automatic resin dispensing and prepared material settings help justify the premium, but finishing, consumables and careful fit checks remain part of the job.

Best atFrequent professional prototypes and small batches with detailed surfaces and a repeatable preparation routine.
Less suited toOccasional hobby models, wide enclosures and buyers trying to minimize equipment and running costs.
The Key Specs
| Build space | 200 × 125 × 210 mmThe 125 mm side limits wide parts; allow room for tilt and supports in PreForm. |
|---|---|
| Detail and fit | 50-micron pixelsFine surface detail does not guarantee dimensional accuracy; inspect your own washed and cured sample. |
| Batch printing | Exposes a whole layer at onceSeveral short parts can share layers, making a filled platform an efficient use of printing time. |
| Routine setup | Automatic resin dispensing, heating and prepared material settingsReduces routine preparation, but supports still need inspection. |
| Finishing | Washing, drying and material-specific curingPrint time is only part of the turnaround; support removal and smoothing still take hands-on work. |
Which Version Should You Buy?
- Form 4 with compatible finishing equipment
- Choose the standard printer for supported prototyping and engineering resins. Check whether the package includes Form Wash, Form Cure and the Flex Build Platform.
- Form 4B
- Consider it when your intended application needs materials unavailable on the standard Form 4; verify the exact printer, resin and intended-use compatibility.
- Open Material Mode add-on
- Choose it for material development or other manufacturers’ resins. The separate per-printer license gives up automatic dispensing, resin-level detection and tank-lifetime warnings.
Budget beyond the printer. Allow for resin, replacement tanks and mixers, washing solvent, gloves, eye protection, ventilation and waste disposal, plus washing and curing equipment where needed. Dedicated tanks make regular resin changes easier but cost more. Supports, failed parts and a replaceable Light Processing Unit add to running costs; service plans and Open Material Mode are additional purchases.
More Specs And Ownership Details
| Starting materials | Grey V5 for shape, fit and presentation; Tough 1500 V2 for parts needing flexibility; Clear V5 for seeing inside prototypes. Match properties and curing conditions to the job. |
|---|---|
| Tall-part removal | Prints taller than 190 mm require removing the resin tank to take the print out. |
| Software | PreForm is free, with automatic and editable supports and a Print Settings Editor. Dashboard and the camera allow remote progress checks. |
| Tank upkeep | Store spare tanks level, covered and protected from light; inspect monthly and after failures. |
| Form 3 upgrade | Form 3-generation tanks, platforms and cartridges do not fit. Check existing wash and cure equipment for capacity and supported material schedules. |
| Workspace | Allow about 16 × 18.8 × 33.2 inches for the printer and access, plus space for washing, drying and storage. |
I’d consider the Formlabs Form 4 if you regularly need detailed prototypes or batches of small parts and want less work getting each job ready. Its strongest selling point is the combination of good output, automatic resin handling, and software with ready-made settings for specific materials. Reported tests support that appeal, while also showing that supports, delicate features, and parts that must fit together still need attention.
The biggest drawback is the cost of the whole setup. You’re buying into a system of resin, tanks, finishing equipment, and service, and cheaper consumer resin printers deserve a look if you mainly print for fun. The Form 4 also leaves you with chemical handling and cleanup after the printing stops.
I’d recommend it for frequent professional work once a sample of your own part passes inspection. It’s harder to justify for occasional models, and it can’t guarantee that every part will be the right size.
What The Form 4 Can Make For You
The Form 4 suits detailed housings, presentation models, small fixtures, and prototypes with features that would be difficult to finish neatly on a filament printer, which builds parts from melted plastic fed from a spool. Its stated build space is 200 × 125 × 210 mm, or about 7.9 × 4.9 × 8.3 inches. Wide enclosures may be a tight fit because one side measures only 125 mm.
Load your model into PreForm, Formlabs’ software for preparing print jobs, before deciding it fits. Supports are temporary structures that hold parts during printing and are removed afterward. They take up space, as can tilting the part and the software’s adjustments for resin shrinkage.
Jobs taller than 190 mm also require removing the resin tank to take the print out. A part that barely fits can be awkward to handle afterward.
The printer hardens liquid resin with light, one layer at a time. Formlabs calls its system Low Force Display: a liquid crystal display (LCD) controls where light passes through, exposing a whole layer at once. Several short parts can share those layers, while a tall part needs more layers. That helps explain why a batch can be an efficient use of the printer.
Choose the resin around what the part must do. Grey V5 is a sensible starting point for checking shape and fit or presenting a design. Tough 1500 V2 is a candidate for parts that need to bend without breaking, such as snap-fit enclosures. Clear V5 lets you see inside a prototype.
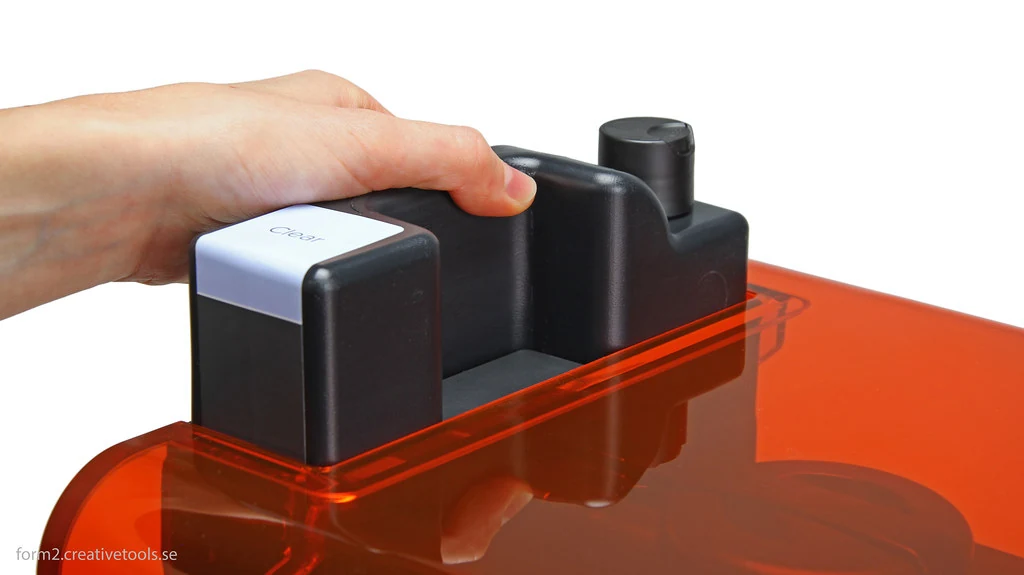
Parts may need further hardening under ultraviolet (UV) light after printing, called post-curing. The curing conditions affect their strength. For parts that need to do more than look good, compare the material’s properties under those conditions with the heat, load, and repeated movement your part will face. A resin described as similar to a familiar plastic isn’t identical to that plastic.
A convincing anatomical model doesn’t establish that it’s safe for patient contact. The standard Form 4 and the Form 4B don’t allow all the same materials; check that the exact printer and resin support your intended use before buying.
How Well Form 4 Prints Look And Fit
The Form 4’s detail is convincing. In a reported test, an AmeraLabs Town model printed in Grey V5 in layers 50 microns (0.05 mm) thick using default settings had particularly clean small features. That’s useful evidence for models with lettering, fine textures, and small surface details. It doesn’t tell you whether two large enclosure halves will meet neatly around every edge.
The printer’s 50-micron pixel size describes its light pattern, not a guaranteed error limit. A hole can look round but still be too small. A smooth wall can be slightly bowed. The resin, the angle at which you print the part, its supports, and finishing all affect the result.
One independent test printed twelve copies of a measurement model. Their measured dimensions differed from the intended dimensions by about 0.048 mm on average. The reported standard deviation, a measure of how much the measurements varied, was about 0.016 mm. Those results are encouraging for repeated copies of that shape, but an average error isn’t a maximum error.
Holes also had errors in their vertical dimensions, attributed to trapped resin or hardened resin where supports touched them. The report doesn’t give the full resin, print orientation, and finishing details for those measurements, so it doesn’t establish an error limit for your parts.
Formlabs’ own dimensional tests have clearer conditions: Grey V5, 100-micron layers, and a five-minute room-temperature post-cure, using one test model across three printers. The results are a starting point for evaluating similar parts. They don’t promise the same fit in another resin, on a different shape, or after a different cure.
Threaded parts may need extra work after printing. Another hands-on report found that small #10-32 UNF threads needed cleaning up with a tap, the tool used to cut internal threads.
That report also encountered warped complex parts and improved most by printing them vertically. It didn’t tie those results to a complete resin and curing recipe, so printing vertically is something to try, not a universal fix.
Delicate parts need care too. In an independent test of a detailed Grey V5 figure, supports were difficult to remove cleanly even after the points where they touched the figure were reduced to 0.35 mm. Making those points smaller doesn’t necessarily make them easy to reach or prevent damage during removal.
For a display model, inspect visible surfaces and allow time to smooth support marks. For parts that must fit together, request a sample of your most demanding representative part, including its holes, threads, thin walls, and surfaces that meet other parts. Check it after the intended wash and cure, then check repeated copies if you’re planning production.
How Long It Takes To Get A Finished Form 4 Part
The Form 4 can make another design revision possible during the same working day, but your model and resin decide whether that happens. The reported Grey V5 AmeraLabs print took 44 minutes at 50-micron layers. A much larger character bust at the same layer height and default settings took four hours and 59 minutes. Both are printing times, with finishing still to come.
Batches can make good use of the Form 4’s speed. A reported PreForm comparison estimated roughly 72 minutes for nine Benchy boat models with supports, alongside 74 minutes for one supported boat at 100-micron layers. These were software estimates, not measured times for a finished batch.
The slightly shorter batch estimate doesn’t prove that adding parts makes printing faster. It shows that filling the platform needn’t multiply printing time by the number of parts.
You still need to position the models in PreForm, inspect supports, and prepare the printer. After printing, you’ll wash away leftover liquid resin, let the parts dry, remove supports at the stage specified for your material, and complete any required UV post-cure. Support removal and smoothing visible marks take hands-on work even when the wash and cure cycles run unattended.
Grey V5 provides a useful example. Formlabs lists a five-minute wash and recommends a short post-cure, although post-curing is optional for this general-purpose resin.
Its published material data include a five-minute room-temperature cure and a different, heated cure. The cure you choose changes the strength you can expect. Drying and handling also prevent you from simply adding ten minutes to a print estimate and calling the part finished.
Engineering materials can take longer. For Tough 1500 V2, Formlabs recommends at least ten minutes of air drying before handling for the best surface finish. Its published mechanical data use a twelve-minute cure at 70°C in Form Cure V2. Use the instructions for your resin version and curing machine, rather than copying a general-purpose resin schedule.
Think about where you’re losing time now. If you’re waiting overnight for prints, shorter jobs can help. If sanding, painting, or inspection consumes most of the day, a faster printer may change less. For batches, check how many parts your wash and curing equipment can accept together; the printer’s full platform isn’t automatically one finishing batch.
How Much Attention The Form 4 Needs
The Form 4 removes several routine chores. Its touchscreen guides setup, and its normal cartridge workflow dispenses resin automatically. Heating and sensors help control printing conditions. That makes it easier to hand a prepared job to a colleague, although someone still needs to understand resin handling and recognize a questionable setup.
PreForm can choose a printing angle for models and generate supports. You can also edit supports manually. Inspect where they touch your part, especially around holes and surfaces that must fit against something else. Automatically placed supports may hold the part successfully but be difficult to remove afterward.
PreForm’s free Print Settings Editor lets you change settings such as light exposure and layer height. You can also hollow out models and add holes for resin to drain out. Software updates have changed support settings and added controls intended to improve threads and downward-facing features. Save the settings used for a successful production job, and check another sample when changing them.
Supports explain some conflicting reliability reports. One hands-on review encountered about five failures with models supplied with their own supports, then reported no failures after switching to PreForm-generated supports. It didn’t give a clear job count for that successful run.
Another review had automatically generated supports detach in clear resin and fixed the problem by adding more contact points. Neither outcome means you can skip inspecting supports.
The advertised 98.7% success rate also needs context. An outside laboratory obtained it over 225 prints across five Form 4 printers, using Grey V5 at 100-micron layers and PreForm-generated supports. Formlabs defined the procedures, and the model shapes were checked beforehand.
Prints could pass despite some cosmetic or dimensional defects. The result supports the printer’s ability to complete those prepared jobs; it doesn’t promise that 98.7% of your parts will meet your inspection requirements or establish long-term reliability.
Formlabs’ Dashboard software and the camera let you check progress remotely, but they can’t inspect a hole or remove a failed print. Failed prints can leave loose hardened resin in the tank, where it can damage the tank’s film. You’ll need to remove that debris and inspect the tank before restarting. Follow Formlabs’ tank-cleaning instructions; draining and filtering the liquid resin may also be necessary.
Tanks need care even when you print occasionally. Keep spare tanks level, covered, and protected from light, including light entering through the underside. Label them by resin and first-use date.
For long storage, follow Formlabs’ instructions for transferring resin to a suitable opaque container. Inspect the tank monthly and after failures.
If you’re buying used, check for a known hinge problem: some early printers assembled before May 4, 2024 have defective cover hinges that won’t hold the lid open. Formlabs provides replacement kits for affected units. This notice concerns those early printers; it doesn’t establish a problem with all Form 4 hinges.
What You Pay For Beyond The Form 4 Printer
The Form 4 costs substantially more than a typical consumer resin printer. When comparing costs, include washing, curing, and the materials you’ll actually use with either printer. The Form 4’s higher cost is easier to justify when you regularly use its prepared material settings and automation.
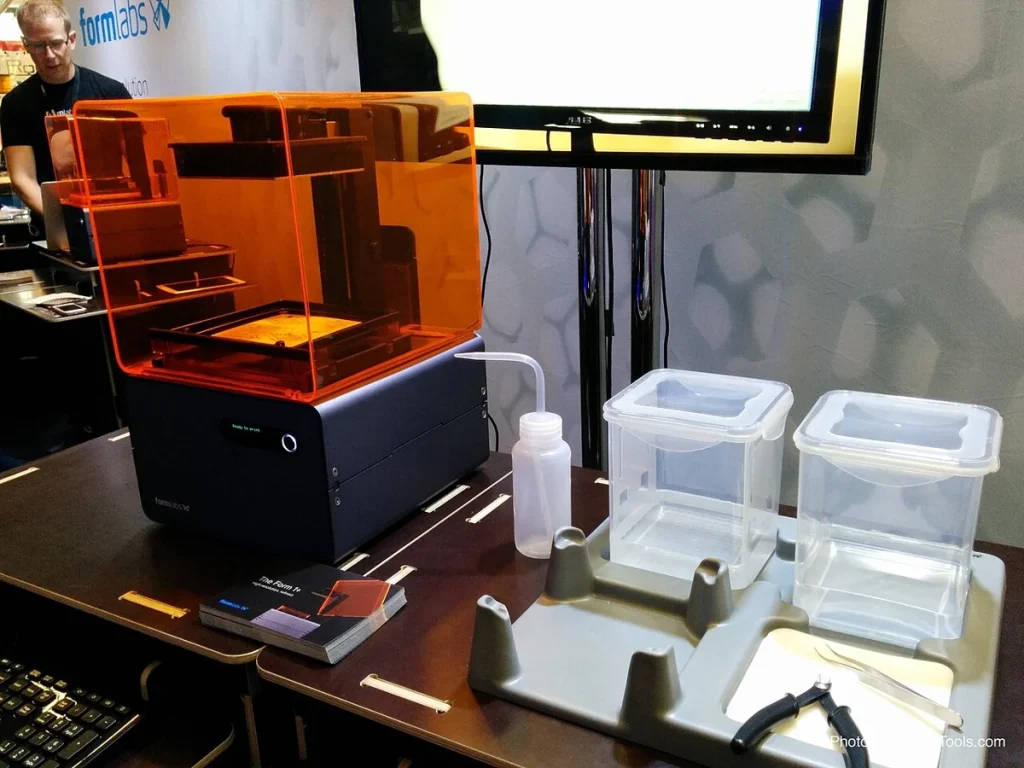
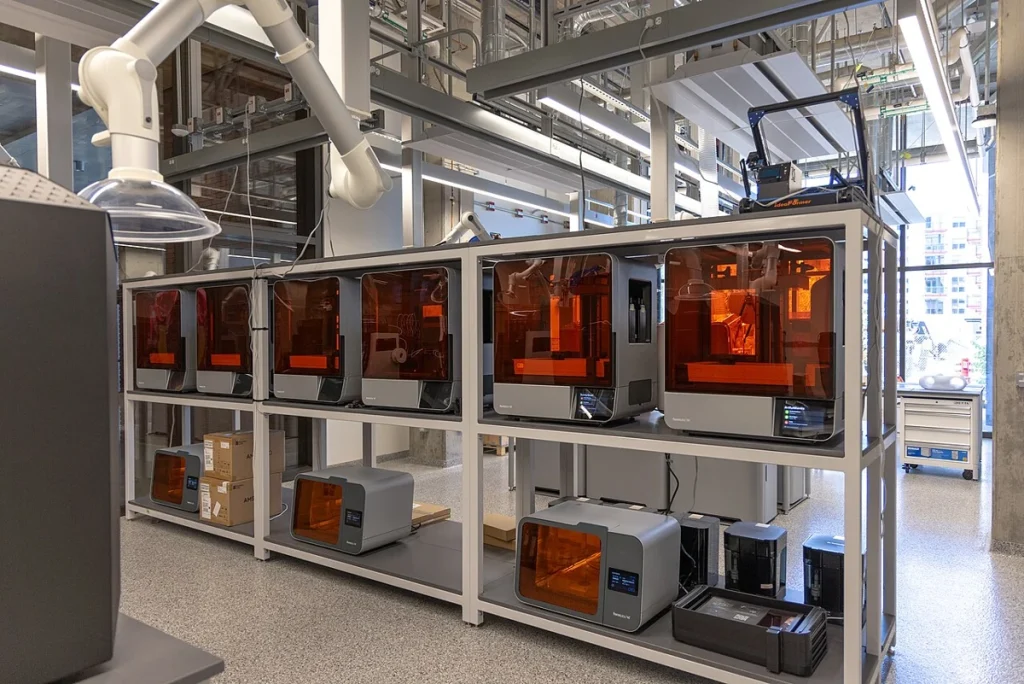
Form Wash automates washing, and Form Cure provides controlled UV post-curing, but they aren’t included in every configuration. The Flex Build Platform is another useful option: prints attach to it during printing, and its flexible surface helps release them afterward. Check the package contents rather than assuming every accessory shown in a product photo comes with the printer.
Resin is only part of your running cost. Tough 1500 V2 costs more per liter than general-purpose Grey V5 in comparable one-liter packaging. Supports, failed jobs, and resin lost during handling also count. Divide your actual material use by the number of acceptable finished parts, not just the number the printer completed.
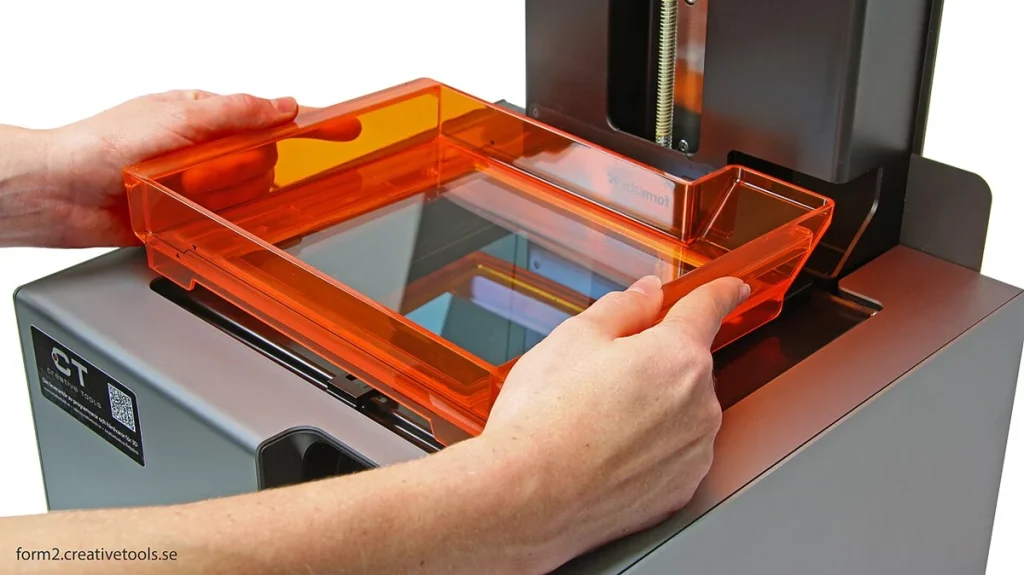
Tanks need replacement too. Formlabs estimates tank life at 75,000-plus layers, subject to wear and damage; reaching that count doesn’t force immediate replacement. With some materials, tank wear can cause surface defects before then. Replace a damaged tank or one whose wear spoils your parts.
Each tank also needs a mixer, a moving part that keeps the resin evenly mixed during printing. Formlabs recommends replacing it with the tank as routine upkeep; that doesn’t mean both always wear out together. A mixer needs replacement if it’s visibly damaged, leaves debris, or discolors the resin.
Keeping a tank and mixer for each regularly used resin saves you from cleaning the old resin out of both before a change. That reduces the work needed to keep different resins from mixing, but means buying more equipment.
The Light Processing Unit (LPU), which contains the LCD that shapes light into each printed layer, also wears out and can be replaced. Formlabs says it should last at least a year under average use, but could last closer to three months in high-volume production. Those are manufacturer expectations, not independently measured replacement intervals. If you plan to print in high volumes, account for that possible replacement frequency when budgeting for spares and service coverage.
PreForm itself is free. To freely use resins from other manufacturers on the standard Form 4, you need to buy a separate Open Material Mode license for each printer. It’s a one-time purchase.
That mode also disables automatic dispensing, resin-level detection, and tank-lifetime warnings. You’ll manage filling and settings yourself. It can suit material development, but buying it to save on resin gives up some of the automation you’re paying for.
Formlabs hardware carries a one-year factory warranty, with paid service plans offering additional coverage. Check the exclusions for individual components: its LPU lifetime-failure coverage excludes printing with Open Material Mode. That exclusion doesn’t mean resin from another manufacturer voids every part of the warranty, but you shouldn’t assume all failures are covered either.
If you’re upgrading from the Form 3 generation, you need Form 4 tanks, build platforms, and cartridges; the older versions don’t fit this printer. An original Form Wash can wash detached parts that fit its basket, but doesn’t accept the Form 4 platform. An existing Form Cure V1 can remain useful where the part fits and the resin has a supported V1 curing schedule. Check capacity before replacing equipment or assuming you can reuse everything.
You’ll also need space to work safely. Allow about 16 × 18.8 × 33.2 inches for the printer and access to it, plus room for washing, drying, and storage.
Provide ventilation for printing and finishing, wear splash eye protection, and use gloves suitable for both resin and solvent. Keep isopropyl alcohol (IPA), the washing solvent, in closed containers and away from ignition sources.
Collect resin-contaminated solvent for appropriate disposal; never pour it down the drain. Businesses must arrange disposal under the rules applying to their waste.
Check the batch number on your resin too. Formlabs identifies Tough 1500 V2 lot 20250827 as having reduced toughness and offers compensation for affected purchases. Don’t use that lot to judge the material’s normal performance.
When The Form 4 Makes Sense For Your Work
For frequent prototypes and small production runs, the Form 4 is a strong choice when you need detailed surfaces and a supported resin meets your parts’ strength, flexibility, and heat requirements. Its software, automatic resin dispensing, and finishing options are especially useful when several people need to follow the same printing routine.
Request the print settings and curing conditions with your sample so you know how the result was achieved. For production, include cleanup, inspection, rejected parts, consumables, and staff time in your cost estimate. Time saved only helps repay the premium if it frees someone for useful work or lets you complete jobs sooner.
If you print miniatures or decorative objects occasionally, a cheaper consumer resin printer is the closest alternative. You still need the finishing space and chemical precautions, and you’ll need to assess its supports and material settings. But an occasional hobby workload makes the Form 4’s higher equipment cost harder to justify.
For larger brackets, rough prototypes, or parts better suited to a familiar plastic available as filament, consider filament printing. It avoids the liquid-resin wash-and-cure process, though it has its own ventilation needs and surface-finish tradeoffs.
If you already own a Formlabs printer, upgrade when print queues, material needs, or hands-on work are limiting you. Keep a working printer if it already meets your deadlines and quality requirements. The Form 4 is worth paying for when it makes acceptable parts easier to produce often enough to matter to you.


