NinjaFlex Review
Less upfront for a small spool; larger Snow White 1.75 mm spools cost less per kilogram.
Our verdict
I’d choose NinjaFlex for soft covers and prototypes that need to bend or squeeze easily. Its 85A TPU needs a well-supported feed path and patient tuning; I would choose a firmer TPU first when a little give is enough.

Best atSoft covers and flexible prototypes where the extra softness justifies slower printing.
Less suited toQuick, load-and-print jobs or printers without confirmed support for soft 85A TPU.
The Key Specs
| Material / feel | TPU, Shore 85ASofter than 95A TPU; walls and infill still determine how readily the part squeezes. |
|---|---|
| Feeding | Soft filament needs a supported pathDirect drive helps, but gaps near the drive gears can still let it buckle. |
| Printing pace | 10–20 mm/s top/bottom; 15–35 mm/s infill and wallsNinjaTek’s starting ranges favor patient printing; tune them for your printer. |
| Nozzle / bed | 225–250°C / room temperature–50°CManufacturer starting ranges; follow your build plate’s preparation instructions. |
| Diameter | 1.75 mm or a listing labeled 3 mmMatch your printer; confirm the actual spool diameter if your machine specifies 2.85 mm. |
Which NinjaFlex Spool Should You Buy?
- 0.5 kg spool
- Choose a smaller amount while establishing compatibility and testing your intended design.
- 1 kg or 2 kg spool
- Choose more material once the printer and profile are proven; check the available diameter and color combination.
Budget for preparation and trial prints. Allow spare filament for small trials and restarts, plus glue stick or blue painter’s tape where your bed instructions call for it. Setup time is part of the cost.
More Material And Handling Details
| Exact grade | This review covers original NinjaFlex 85A. NinjaFlex Edge 83A is a separate material. |
|---|---|
| Cooling | NinjaTek recommends the print-cooling fan from layer two onward, if available. |
| Storage | Keep in the original container under normal room conditions; obtain NinjaFlex-specific drying instructions before heating a spool. |
| Part geometry | Bridges, steep overhangs and trapped supports make flexible prints harder; simple shapes reduce cleanup demands. |
| First sample | Check feed consistency, bed release, fit and recovery using the intended wall thickness; a short trial does not establish long-term durability. |
I’d consider NinjaFlex when you want a part that feels soft, bends easily, and has some spring to it—and you’re willing to slow down to get it printed. Its biggest drawback starts before the part takes shape: the filament is soft enough to bend inside a poorly supported feeder instead of moving toward the nozzle.
I’d choose it for a project where that softness matters. If you just need a little give, a firmer TPU such as NinjaTek Cheetah 95A is worth considering first. NinjaFlex needs a suitable printer and patient setup, so it’s a less appealing first flexible filament if you expect to load a spool and press print.
How Soft Do Your NinjaFlex Parts Need To Be?
The original NinjaFlex is thermoplastic polyurethane, or TPU, with a Shore hardness of 85A. That hardness rating describes how much the material resists being indented. A lower number on the same scale means a softer material, so NinjaFlex is softer than a 95A TPU. It isn’t a percentage: 85A doesn’t mean “85% flexible.”
Make sure you’re buying the intended grade. NinjaTek still lists NinjaFlex 85A alongside NinjaFlex Edge 83A, which is a separate product. The similar names don’t make their settings or test results interchangeable.
Softness, stretch, and recovery answer different questions. Softness tells you how readily a material gives under pressure. Stretch describes how far it extends when pulled. Recovery is how well it returns after you let go.
NinjaTek’s technical sheet lists 660% elongation at break, but that describes a test specimen stretched until failure. It doesn’t promise that your printed part can repeatedly stretch that far and return unchanged.
One reported 2014 print gives a useful example: a bracelet with a single 0.4 mm wall, made on a BAM Makeblock printer, reportedly stretched to roughly five to eight times its original length before snapping. That’s an informal demonstration of stretch, not a measured strength or service-life result.
Your design matters, too. Thicker outer walls and more infill—the pattern of plastic inside the part—generally make it harder to squeeze. Thin walls and a more open interior allow more movement.
A soft filament won’t make a thick, nearly solid block feel like a hollow squeeze toy. For a soft cover or flexible prototype, test the wall thickness you actually intend to use.
Can Your Printer Feed NinjaFlex Reliably?
Check your printer’s guidance for soft TPU around 85A, rather than stopping at “TPU supported.” A printer may handle a firmer grade while needing a different loading route or settings for NinjaFlex.
Start with the extruder, the mechanism that grips and pushes the filament. In a direct-drive setup, it sits close to the heated nozzle assembly. A Bowden setup pushes filament through a longer tube before it reaches that assembly.
The shorter push in direct drive is helpful, but the filament still needs support between the drive gears and the entrance to the heated section. An open gap gives it room to buckle.
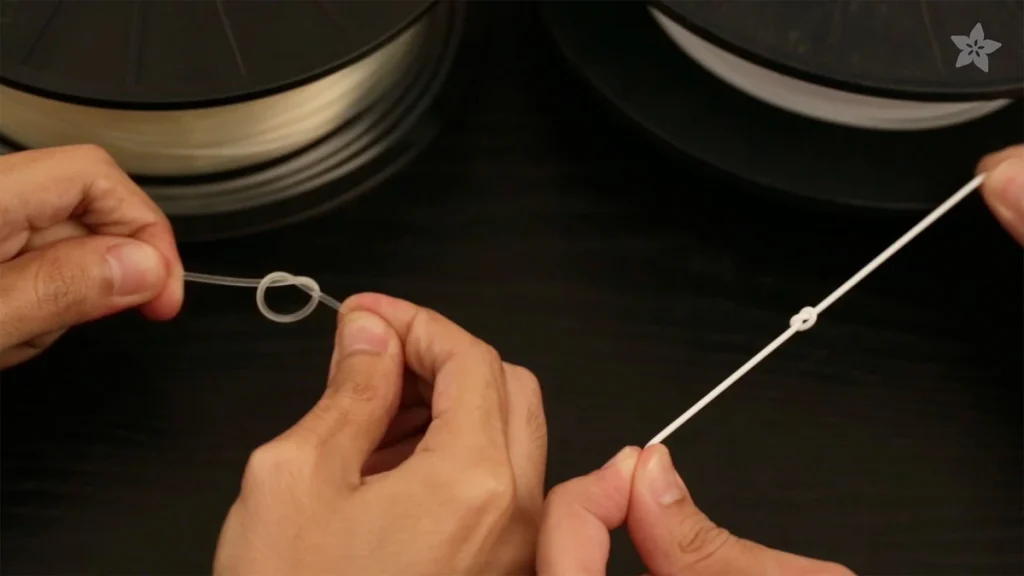
That distinction showed up in the historical BAM test. Even with its direct-drive Bulldog XL extruder and Hexagon heated nozzle assembly, the tester reported filament curling inside the extruder above 30 mm/s. That’s a limit observed on that setup, not a speed ceiling for every printer. It also shows why direct drive alone isn’t a guarantee.
Check the entire loading route, including any automatic spool feeder. For example, Bambu Lab’s P2S manual lists 85A TPU as supported through the inlet on the printhead, while marking it incompatible with the AMS automatic feeder. That confirms support for this hardness, but you’ll still need suitable settings for NinjaFlex. Follow the instructions for your exact printer and feeder combination.
Match the filament diameter as well. NinjaTek lists 1.75 mm and 3 mm options. If your printer specifies 2.85 mm, confirm the exact spool’s diameter with the supplier before ordering; don’t assume a rounded listing label settles compatibility.
If you have a Bowden printer, look for a demonstrated NinjaFlex setup using the same extruder and tube arrangement. Without one, expect experimentation. A historical failure on another machine doesn’t prove yours can’t print it, but generic TPU support doesn’t establish that it can.
What It Takes To Get A Clean NinjaFlex Print
Expect to use slower print settings than you would for ordinary rigid filament. NinjaTek suggests a nozzle temperature of 225–250°C and a print bed from room temperature to 50°C. Its recommended speeds are 10–20 mm/s for top and bottom layers, and 15–35 mm/s for infill and outer walls.
It recommends using the print-cooling fan from the second layer onward, if your printer has one. These are starting ranges; your filament diameter, nozzle size, layer height, and printer still matter.
Use a NinjaFlex profile—a saved set of print settings—for your exact printer if one is available. Otherwise, start near the lower end of the recommended print-speed ranges and change one setting at a time. Slower printing reduces the risk of filament tangling in the drive gears.
The old BAM result used 220°C without a fan, differing from today’s manufacturer guidance. Copying that whole recipe onto a different printer would ignore both the hardware and the age of the test.
Retraction needs particular care. This setting pulls filament back when the nozzle moves between printed areas, helping reduce the fine threads called stringing. Soft filament can stretch instead of moving back immediately, so a larger pull doesn’t necessarily give you better control of the flow.
Lower retraction settings can reduce the risk of clogs or filament tangling in the extruder. Follow your printer’s flexible-material guidance; you can start with little or no retraction and increase it cautiously while watching the results.
Clean results are possible. In a printer-maker’s 2023 demonstration, NinjaFlex prints on a LulzBot SideKick 747 using its supplied Cura profile reportedly had almost no stringing. That shows what a suitable setup can achieve, without establishing the same result on other machines.
Plan how you’ll remove the print before starting it. PEI is a plastic used to coat print beds, and soft TPU can grip a smooth PEI surface strongly enough to damage it during removal. A separating layer, such as glue stick, keeps the print from bonding directly to that surface.
NinjaTek suggests glue or blue painter’s tape when printing without a heated bed. For your particular plate, follow its maker’s preparation instructions. Textured PEI can be suitable, so check the specific surface rather than ruling out every PEI plate.
For storage, NinjaTek’s safety sheet specifies the original container under normal room conditions. NinjaFlex can absorb moisture, and wet flexible filament can be harder to print reliably. Get drying instructions specifically for NinjaFlex before heating a spool; a drying recipe for another TPU isn’t automatically suitable.
Is NinjaFlex Worth The Extra Effort?
If your prototype needs to fold or squeeze easily, accepting a slower print may be reasonable. If the finished part only needs a little bend, you have less reason to accept the feeding demands of 85A TPU.
Cheetah 95A is a useful alternative to consider within the same brand. Its higher hardness makes it firmer, and NinjaTek recommends faster printing ranges for it.
Those recommendations suggest more room for speed; they aren’t a measured promise that your part will finish a particular amount sooner. Choose between them for the required feel and your printer’s supported settings, rather than assuming either is universally better value.
The shape of your part can matter more than spool cost. Flexible materials struggle with bridges, where the printer lays plastic across an open gap, and with steep overhangs, where a layer extends far beyond the one below it. Supports are temporary printed structures that hold up these areas, but they can bond too firmly to flexible parts and become difficult to remove.
A simple cover that needs no supports is an easier NinjaFlex project than a part with supports trapped inside hard-to-reach cavities. Consider whether turning the model to print at a different angle or changing its shape could reduce the need for supports.
Compare spool prices for the same diameter and filament weight. There’s no reason to assume NinjaFlex always costs more than a firmer alternative.
Include your own time in the decision: if tuning and restarting a failed print would disrupt workshop jobs, an already proven material and profile may be worth more to you than extra softness.
Should You Choose NinjaFlex For Your Next Part?
Choose NinjaFlex if you need a part that gives easily under pressure, know your printer can feed 85A TPU, and can spend time tuning a small print.
Start with a short section of your intended design that includes its real wall thickness and any holes or bends. Check whether it feeds consistently, releases from the bed, feels right, and returns to shape after the movement you expect.
Skip it for now if your printer maker says it isn’t compatible, or if a firmer TPU already does the job. If compatibility is unclear, check with the printer maker before buying.
That first sample can establish fit and feel. It can’t establish long-term durability or qualify a part for critical loads, protective equipment, or prolonged skin contact. For those uses, you’ll need evidence for the finished part and its actual conditions of use.


