Overture High Speed TPU Review
A small premium over standard Overture TPU for a comparable single-spool purchase.
Our verdict
I’d try Overture High Speed TPU for repeated flexible prints when ordinary TPU takes too long. Start with one spool and a small fit sample: the potential time saving is useful only if the part still bends enough, and this grade may feel firmer than standard TPU.

Best atRepeated flexible parts on a direct-drive printer when you can tune the profile and adjust the design.
Less suited toSoft, squishy parts, Bowden feed paths, or projects that depend on automatic material changes.
The Key Specs
| Reviewed material | High Speed TPU 95A · 1.75 mmCheck that the spool says High Speed; standard Overture TPU is a separate material. |
|---|---|
| Flexibility | Approximately 95A Shore hardnessThe label does not predict how easily your printed part bends; try a small section before committing. |
| Speed guidance | Overture specifies 60–90 mm/sActual time savings depend on flow limits and geometry; compare the same part and settings. |
| Feeding | Direct drive; external-spool route on Bambu printersAvoid Bowden feeding. Original AMS, AMS lite and AMS 2 Pro automatic feeding are unsuitable. |
| Drying | Overture specifies 70°C for seven hoursUse a dryer and spool rated for that temperature, then store sealed with desiccant. |
Which Spool Or Pack Should You Buy?
- 1 kg option
- I’d start here to check the feel and profile before buying more.
- 2 kg option
- Consider the larger quantity once a sample meets your needs; compare equal weights when judging value.
Budget For Drying And Storage. Allow for a suitable filament dryer, sealed storage and desiccant, plus filament for small tuning samples. Add a freely turning external spool holder if needed and the separating glue specified for your build plate.
Also consider: Overture TPU. I’d favor the standard grade when a softer feel matters more than potential speed gains; keep a known-good print as your comparison.
More Handling And Compatibility Details
| Nozzle / bed | 200–240°C nozzle; 25–60°C bed; print-cooling fan on. These are starting ranges, not a complete profile. |
|---|---|
| Part design | Infill, walls and solid layers affect bending. Recheck fit and behavior after reducing them. |
| AMS HT | Generic TPU uses its manual bypass outlet, without automatic loading or color changes; confirm your printer’s routing. |
| Strength evidence | Overture’s published mechanical samples were solid and printed at 30 mm/s; those results do not establish equivalent strength at higher speeds. |
I’d try Overture High Speed TPU if slow flexible prints are tying up your printer and you can accept a part that may feel firmer than ordinary TPU. TPU, short for thermoplastic polyurethane, is a plastic used for flexible prints. This High Speed version’s main tradeoff is potential time savings against a change in how easily your part bends.
This review covers Overture’s High Speed TPU 95A with a filament diameter of 1.75mm, a separate product from its standard TPU 95A. I’d start with one spool and a small test section of the part you need. For something that must feel soft and squishy, I’d favor ordinary TPU, or a softer grade your printer can handle.
How Much Time Could High Speed TPU Save?
Overture advertises printing up to five times faster than standard TPU. Treat that as a manufacturer claim, not a promise that a ten-hour job will finish in two. The published guidance lists printing speeds of 60–90mm/s, but neither figure establishes the time your part will take.
Three different settings can get confused here. Print speed describes how fast the nozzle moves while laying down plastic. Travel speed describes movement between printed areas, when it isn’t supposed to deposit anything. Maximum volumetric speed limits how much melted plastic passes through the nozzle each second, measured in cubic millimeters, or mm³/s.
Thicker layers and wider lines need more plastic at the same movement speed. The slicer—the software that prepares your model for printing—can slow those moves to stay below the flow limit. Raising travel speed alone doesn’t increase that limit.
Owner reports make a more modest improvement plausible. One owner reported roughly halved printing time with a 0.4mm nozzle after changing a generic TPU profile—a saved set of printing settings—to 1mm retraction and 7.2mm³/s maximum volumetric speed. Retraction briefly pulls filament backward to reduce leaking from the nozzle during travel.
Another reported at least twice the speed of standard TPU on the Bambu A1 and A1 mini. Neither supplied a complete comparison with matching parts, settings, finish and measured elapsed time.
Check the slicer’s speed and flow preview before expecting a big saving. Long sections limited by material flow offer more opportunity than tiny features that need cooling or slower movement.
Compare estimated times with the same model, outer walls, internal fill and thickness of each printed layer, then time a sample print. A faster estimate only matters if the finished part still looks and works well enough.
Will Your High Speed TPU Parts Have Enough Flex?
The 95A label describes Shore hardness: how strongly the material resists a standardized indentation test. It doesn’t tell you how much force you’ll need to bend a printed case or squeeze a hollow ball. Overture’s technical sheet lists approximately 95A, but owners have reported a noticeably firmer feel than other filaments carrying that label.
One owner comparing printed airless tennis balls found Overture High Speed much harder to squeeze than Bambu TPU 95A HF. Another who printed with both standard and High Speed Overture TPU also described the High Speed version as stiffer. These are useful reasons to try a sample, but without full print settings or measured hardness, they can’t tell you exactly how the materials compare.
Your design matters, too. Infill is the structure printed inside a part; increasing it generally leaves less room for the part to compress. Outer walls and solid top and bottom layers also resist bending. A thin sleeve and a thick block won’t feel alike simply because they came from the same spool.
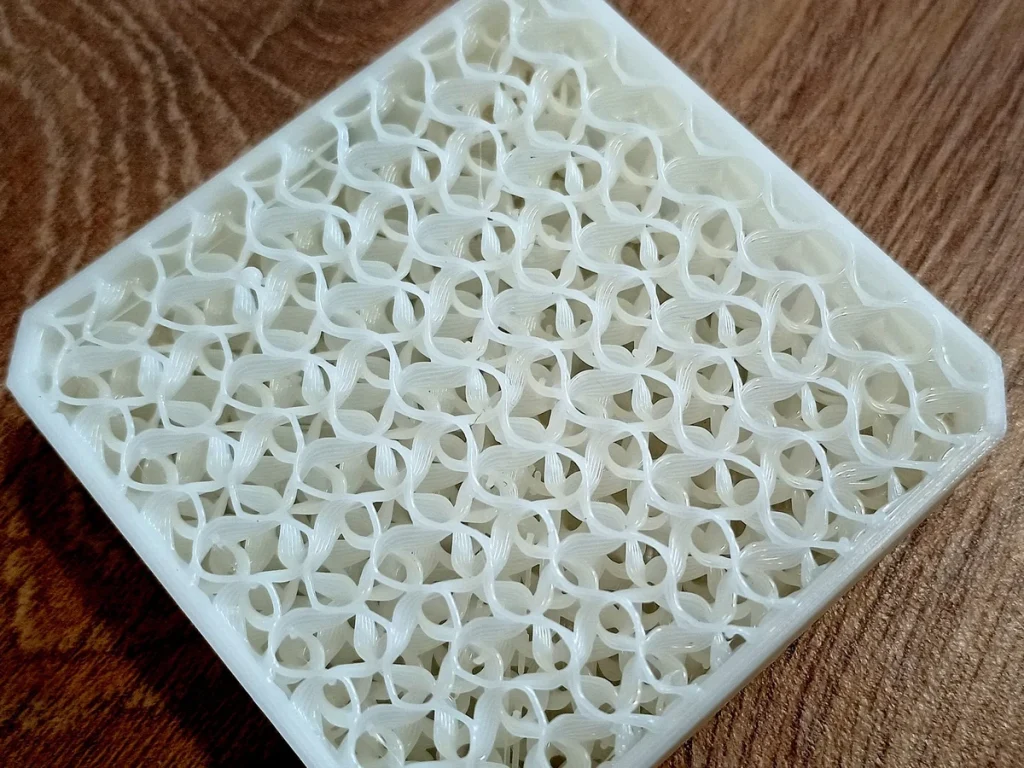
You can try less infill or fewer walls if your first sample is too firm. One owner reported reducing infill to regain some of the flex they got from ordinary TPU. That changes the part’s structure, though, so check its fit and behavior again instead of assuming you’ve made an equivalent replacement.
For a cover that needs to bend over an edge, print the section that needs to bend first. Squeeze or bend it as intended and check whether it returns to shape. A small fit check won’t establish long-term durability, but it can stop you spending hours on something that feels wrong immediately.
Getting Overture High Speed TPU Started On Your Printer
Plan on a direct-drive extruder, where the gears pushing the filament sit close to the heated nozzle. Overture advises against using this filament with Bowden extruders, which push filament through a longer tube. Flexible filament can buckle under that pushing force and jam; a shorter path helps limit that problem.
An external spool holder doesn’t convert a Bowden printer into direct drive. Keep the spool turning freely and avoid unnecessary bends or drag along the route to the extruder, so it doesn’t have to pull against extra resistance.
For Bambu printers, use the external-spool route specified for your machine. Overture excludes the original AMS and AMS lite automatic filament feeders; Bambu also excludes generic TPU from AMS 2 Pro automatic feeding.
The AMS HT has a separate manual bypass outlet for generic TPU. That doesn’t provide automatic loading or color changes. Confirm the bypass routing for your printer before using it.
Dry the filament before printing: TPU absorbs moisture from the air, which can cause rough surfaces and unwanted strands between printed features. Overture specifies 70°C for seven hours for High Speed TPU. Check the instructions supplied with your exact spool, and use equipment and a spool rated for the specified temperature.
Don’t assume extra hours at a lower temperature are equivalent. Store dried filament sealed with desiccant, which absorbs moisture.
The High Speed technical sheet gives a 200–240°C nozzle range, a 25–60°C bed range and the print-cooling fan switched on. These are starting ranges, not a complete profile.
To remove prints, follow the build plate maker’s TPU guidance: Bambu’s Dual-Texture PEI plate instructions specify glue on both surfaces and cooling before removal. Here, glue provides a separating layer so the flexible print doesn’t bond too strongly to the surface.
On an A1 or A1 mini, the Bambu TPU 95A HF filament preset is worth trying on a small print: owners reported success with it unchanged. That report didn’t establish the same result on a P1S.
Choose the preset for your actual printer and nozzle, save a copy named for Overture, and check its temperatures before printing. Don’t import an entire project from a different printer and assume every setting transfers.
Where I’d Be Cautious With High Speed TPU
Stringing—fine strands between printed features—is the first issue I’d investigate when a copied profile gives poor results. An A1-series owner reported substantially more stringing after copying P1P/P1S settings, despite using 1mm retraction and a 7.2mm³/s flow limit. Other A1 owners reported success with the Bambu HF preset. That makes the copied setup a sensible place to investigate, without establishing a single cause.
Start from the correct printer preset and change one setting at a time on a small sample. Check drying, temperature and retraction. Lowering temperature can reduce strings, but going too low can interrupt flow. Stay within the High Speed temperature guidance rather than repeatedly increasing retraction to chase every strand.

Thin edges deserve their own test. A P1S owner reported defects near their tops at 230°C and 8mm³/s, although a Benchy boat model printed acceptably with the Bambu preset. Another owner reported missing segments after drying at 54°C for 11 hours. No confirmed follow-up established the cause or a fix.
For gaps, check whether the slicer preview includes the missing line before changing filament settings. If it does, check spool resistance and the nozzle for obstruction using your printer’s maintenance instructions.
Try reducing the maximum volumetric speed, too: that lowers the amount of plastic the printer must deliver per second on moves that reach the limit. If the gaps improve, the original flow request may have been too high. These checks aren’t proven cures for those particular reports.
Bridges and overhangs—sections printed across gaps or beyond the layer below—can need separate attention. One owner reported better results after tuning an X1C-based profile, including temperature and movement settings. A clean simple model therefore doesn’t establish clean thin edges or unsupported sections. Nor do these scattered reports establish how often defects occur or whether the formulation changed.
Is Overture High Speed TPU Worth Trying For Your Parts?
I’d try it for repeated flexible prints when ordinary TPU takes too long, you have a suitable feed path and dryer, and you can adjust the design if the result feels too firm. A removable cap or a flexible fit prototype gives you something concrete to judge: does it bend enough to install, hold its shape afterward and finish soon enough to make the switch worthwhile?
If your ordinary TPU already gives you exactly the feel you need, keep it as your comparison. For a softer result, a lower-hardness TPU makes more sense, although softer filament can be harder to feed. If automatic material changes are essential, choose a filament explicitly supported by your particular feeding system.
Compare equivalent spool weights when deciding what to spend. A cheaper spool won’t help if its parts are too firm, and paying more for speed only makes sense if you can use that speed.
Don’t assume faster prints will be equally strong: Overture’s published mechanical results come from solid samples printed at 30mm/s, below its recommended 60–90mm/s printing range. For seals, protective equipment or parts exposed to repeated demanding loads, the owner reports don’t establish suitability.


