Prusa MINI+ Review
Costs more to get started than the Bambu Lab A1 mini; the MINI+ package includes an enclosure.
Our verdict
I’d choose the MINI+ for small parts if clear repair guides, replacement parts and familiarity with PrusaSlicer matter more than effortless setup. The enclosure bundle adds appeal when you have a use for it, but you still adjust first-layer nozzle height yourself. For a beginner making small PLA and PETG objects, I recommend the less expensive A1 mini.

Best atSmall PLA and PETG projects, especially as a second printer for someone already using PrusaSlicer.
Less suited toLarge one-piece prints, very soft flexible parts, or beginners who want automatic nozzle-height setup.
The Key Specs
| Print area | 180 × 180 × 180 mmSmall cases and organizer trays fit; oversized parts need splitting, and supports also take up space. |
|---|---|
| First layer | Mesh bed leveling; manual nozzle-height adjustmentRun the first-layer test and save a separate setting for each steel sheet. |
| Material fit | Start with PLA or PETGVery soft flexible filament is harder to feed; abrasive additives need a wear-resistant nozzle. |
| Enclosure space | About 16.9 × 19.7 × 18.5 inchesAllow extra room for the door, cables and external power supply. |
| Repair support | Illustrated guides and individually sold replacement partsYou can find instructions and parts when belts, fans or filament guide tubes need attention. |
Which Version Should You Buy?
- Semi-assembled MINI+ enclosure bundle
- The current direct-purchase option. Choose it if you want the enclosure and are comfortable finishing assembly; the enclosure itself arrives as a kit. A smooth sheet and filament sensor are included.
- Discontinued full printer kit
- Consider remaining dealer stock only if you want a much larger assembly project; confirm the actual package contents before buying.
Budget beyond the printer. Allow for filament, a textured sheet for frequent PETG printing, and the optional Wi-Fi module if Ethernet is impractical. A separate camera and enclosure filtration cost extra. Abrasive filament needs a suitable wear-resistant nozzle.
Also consider: Bambu Lab A1 mini. Costs less, has the same print area and sets nozzle height automatically. I’d choose it for a beginner’s small PLA and PETG projects; its basic package has no enclosure.
More Specs And Ownership Details
| Temperature limits | Nozzle up to 280°C; bed up to 100°C. Check the exact filament’s drying, temperature and sheet requirements. |
|---|---|
| Files and networking | USB printing and Ethernet; Wi-Fi needs an optional ESP module. Keep a USB drive inserted for network uploads. |
| Remote viewing | PrusaLink provides local browser access; Prusa Connect offers internet management. Seeing the print requires a separate camera. |
| Input Shaper | Use updated firmware and PrusaSlicer, then slice again with a MINI+ Input Shaper profile; an old print file will not become faster just from a firmware update. |
| Print sheets | The included smooth PEI sheet suits PLA. PETG on smooth PEI needs the recommended glue-stick separator; save a first-layer setting for each sheet. |
| Upkeep | Check belts, feeder debris and guide tubes. Prusa recommends cleaning and lubricating smooth rods after roughly 200 printing hours. |
I’d consider the Prusa MINI+ if you want to print small parts and value clear repair instructions, replacement parts and control over your print settings. It’s especially appealing as a second printer if you already use PrusaSlicer, the software that turns 3D models into printing instructions.
Its biggest drawback for a beginner is that you still have to adjust the height of the nozzle, which lays down the plastic. The cheaper Bambu Lab A1 mini handles that automatically.
The buying options have changed: Prusa now sells the semi-assembled MINI+ with an enclosure and has discontinued the full printer kit. Think about whether you’ll use that enclosure and where you’ll put it.
Will Your Prints And The MINI+ Fit Your Space?
The MINI+ can print within a 180 × 180 × 180 mm space, or roughly 7.1 inches in each direction. That suits small electronics cases, knobs, model buildings and individual organizer trays. A full-size helmet or a wide drawer insert will need to be printed in smaller pieces and put together.
Check your actual model in PrusaSlicer before buying. Turning a long, narrow part diagonally may help, but it doesn’t make every oversized object fit. Extra plastic printed to hold up overhanging sections, called supports, also takes up room on the printing plate. So does a brim, the extra border that helps a print stick to the plate.
The bare printer measures about 15 inches wide, 13 inches deep and 15 inches tall, excluding its separate spool holder and power supply. You’ll need more desk space than those measurements suggest. The printing bed moves forward and backward, cables need room to bend, and filament—the plastic strand wound onto a spool—needs a clear path into the printer. Prusa recommends placing the spool beside the screen to save space.
With the included enclosure, you’ll need more room: the box measures about 16.9 inches wide, 19.7 inches deep and 18.5 inches tall. Allow additional space for the external power supply, cables and opening the door. A narrow shelf that fits the bare printer may be too small for the enclosed setup.
Getting The MINI+ Ready For Its First Print
The semi-assembled MINI+ still needs some work before you can print. You join its main sections, attach the screen and connect cables. The illustrated instructions show the order and how to line up the parts. Set aside uninterrupted time to follow them.
The enclosure also arrives as a separate assembly kit.
The discontinued printer kit involved building the printer from individual parts. If you find remaining dealer stock, expect a much bigger assembly job.
After assembly, the printer runs startup checks for movement and heating. The SuperPINDA sensor measures the bed at several points so the printer can adjust for small height differences while printing. This is called mesh bed leveling. You still need to set the gap between the nozzle and the printing surface so the first layer of plastic goes down evenly.
During the first-layer test, turn the control knob to adjust the nozzle height while watching the plastic: neighboring lines should join into an even patch. Gaps suggest the nozzle is too high; ridges and excessive flattening suggest it’s too low. You may need to repeat the test to get it right. Use the pictures in the instructions to judge the result instead of copying someone else’s numerical setting.
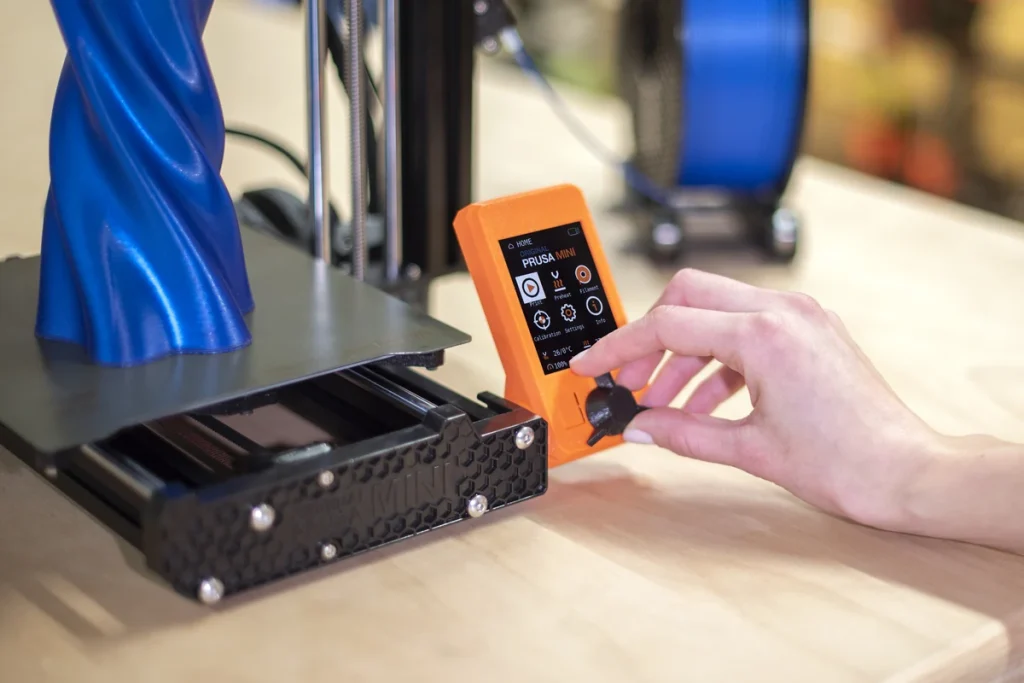
The printing surface is a removable steel sheet, and different sheets can have different thicknesses. Run the first-layer test for each one and save its nozzle-height setting in a sheet profile. Select that saved profile when you swap sheets. Recheck the first layer after a nozzle change or work that alters the nozzle’s position.
The main improvement over the original MINI is the SuperPINDA sensor. Prusa says temperature changes affect its measurements much less, helping the first layer come out more consistently. You still set the nozzle height yourself on either version.
Print results from an original MINI upgraded with SuperPINDA are relevant to the MINI+, too. The MINI+ also changed the clips that hold its bearings, but Prusa says those ease assembly without improving print quality.
What The MINI+ Prints Well, And How Long It Takes
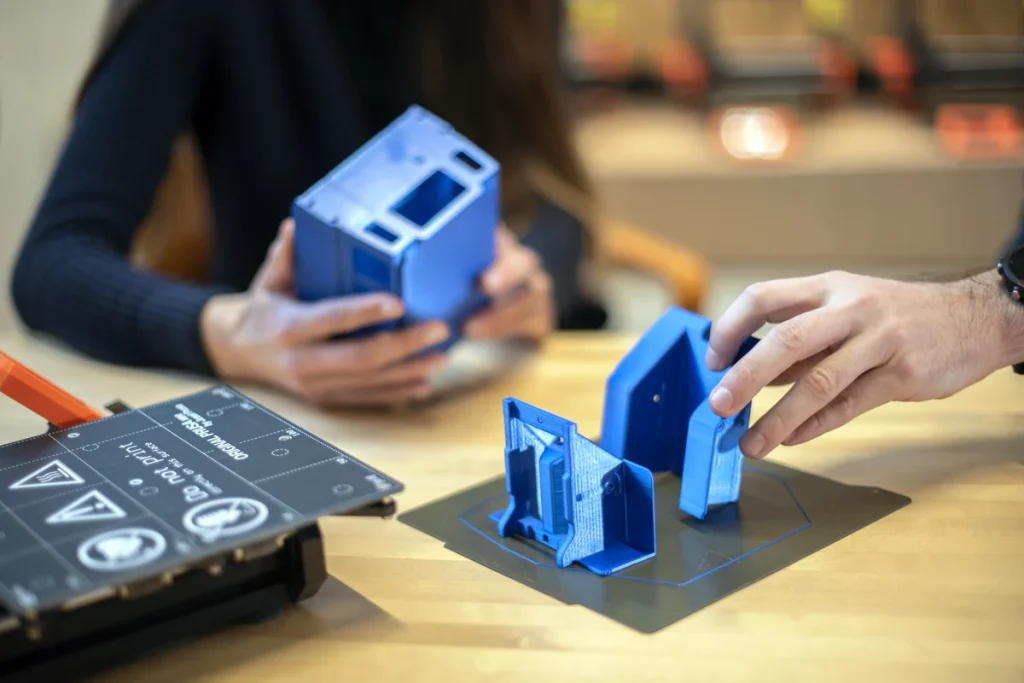
The MINI+ is most convincing for printing with PLA and PETG plastics. PLA is a straightforward starting material for models and household prints; PETG is another common choice for practical parts. Independent MINI+ testing reported successful prints with both Prusa and other brands of these plastics. You don’t have to buy Prusa filament, but you do need settings that match what you load.
One reported test on an original MINI upgraded with SuperPINDA produced a working wind-up car whose gears fit and turned together correctly. Its Benchy boats, small test models with difficult overhanging sections, had little or no stringing: fine plastic threads left behind when the nozzle crosses an empty gap.
The report also showed PETG prints using another brand’s filament, although it didn’t fully record the nozzle, print settings or firmware—the printer’s control software—for each object. Those results are encouraging for small working parts, but they don’t tell you exactly how closely a print will match its intended measurements.
A separate MINI+ test produced smoothly turning interlocking gears after some stray plastic was trimmed away. A geometric sculpture had more stringing. Adjusting retraction, the setting that pulls filament back during moves across gaps, reduced but didn’t eliminate the threads. Expect occasional cleanup on intricate shapes.
Printing thicker layers can save time at the cost of some quality. Profiles are saved sets of printing settings; in the 0.2 mm Quality and 0.3 mm Speed profiles, the numbers describe each layer’s thickness.
That second test timed a four-inch Thinker model at 7 hours 52 minutes with the Quality profile and 4 hours 22 minutes with the Speed profile, with some loss of quality. This compares two profiles, rather than isolating the effect of layer thickness. The test predates Input Shaper and didn’t fully specify filament, nozzle and firmware, so those timings don’t predict what you’ll get today.
Firmware 5.1.0 introduced Input Shaper, which reduces vibration marks, and Pressure Advance, which adjusts for changes in plastic pressure in the nozzle. To use these features, use up-to-date firmware and PrusaSlicer, then generate a new print file with an updated MINI+ Input Shaper profile.
Installing firmware alone won’t speed up an old print file. For your own projects, compare PrusaSlicer’s time estimates at the quality you need; a printer’s advertised movement speed won’t tell you when a part will finish.
Prusa supports flexible filament, but softer varieties are harder to print: the strand can tangle in the gears that feed it into the printer. Prusa advises slow printing to reduce the risk of tangles and nozzle clogs, and keeping the filament dry because absorbed moisture makes printing harder. I wouldn’t choose the MINI+ primarily for soft rubberlike parts.
The nozzle reaches 280°C and the bed reaches 100°C. The enclosure retains heat, keeping the air around the print warmer as it cools. That helps with plastics that curl during cooling, such as ASA.
Even with the enclosure, nylon and polycarbonate aren’t always easy to print. Check the exact filament’s temperature, drying and sheet requirements. Filaments with abrasive additives can wear the nozzle, so they need a suitable wear-resistant one.
Using The MINI+ Day To Day
In PrusaSlicer, choose the MINI+, your nozzle size and your filament, position the model, then preview the layers before saving the print file. The software is free and open-source, runs on Windows, macOS and Linux, and includes ready-made settings to get you started.
For offline printing, save the file to a USB drive and plug it into the printer. The color screen shows a preview, and you select it with the push-and-turn knob. Menu commands heat the nozzle and guide filament loading or unloading; you still feed the strand into the printer.
You can connect the MINI+ to your network with an Ethernet cable; Wi-Fi needs an optional adapter called an ESP module, installed in the electronics compartment. With current firmware, PrusaLink lets you access the printer in a browser on your local network. Prusa Connect offers internet-based management.
These tools let you upload files, start jobs and check progress. Keep a USB drive inserted to store the files. Connect can begin printing before the whole file has transferred. You’ll need a separate camera to see the print remotely.
After printing, let the part and sheet cool before lifting and flexing the steel sheet to release it. The supplied sheet has a smooth plastic coating called PEI and suits PLA.
For frequent PETG printing, I’d add a textured sheet: PETG can stick firmly enough to damage smooth PEI. If you use the smooth sheet, Prusa’s guidance calls for a thin glue-stick layer as a separator to protect the surface. Follow its material-specific cleaning guidance and keep fingerprints off the printing area.
Don’t count on the MINI+ being quiet enough to sleep beside. Older noise reports don’t establish how the current enclosed setup will sound.
You also need to plan for ventilation: filament printers release particles and gases, and a plain enclosure doesn’t replace suitable ventilation or effective filtration.
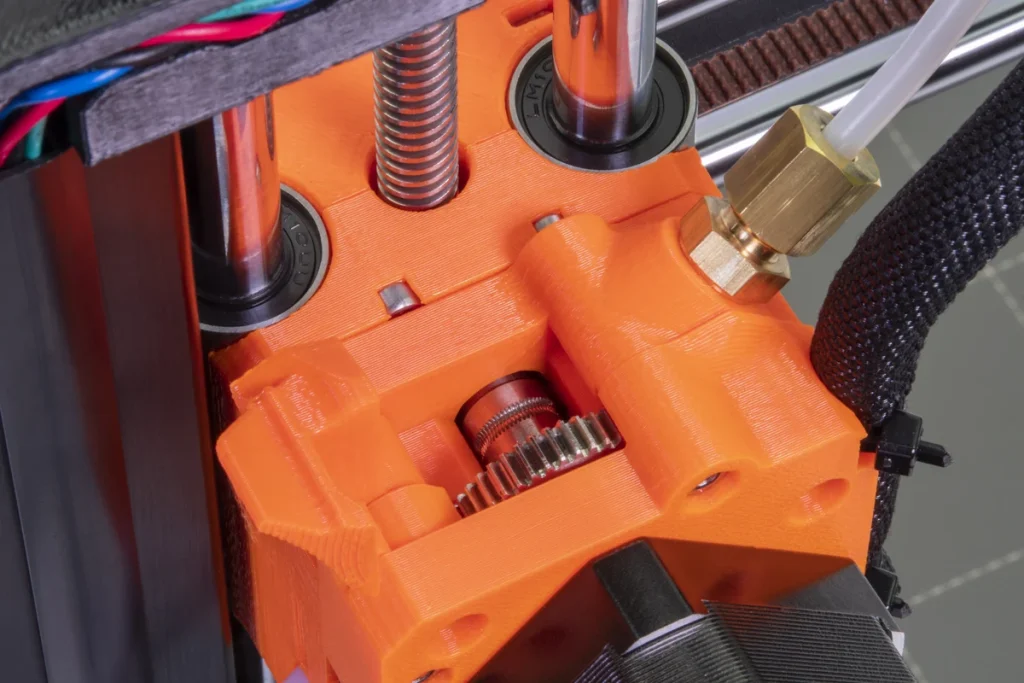
Routine upkeep includes checking belts, clearing filament debris from the feeder and inspecting the plastic guide tubes for wear. Prusa recommends cleaning and lubricating the smooth rods after roughly 200 printing hours. Follow its maintenance guide for the details.
Does The MINI+ Justify Its Cost?
For small PLA and PETG projects, the Bambu Lab A1 mini is the closest alternative I’d consider. It costs less to get started, offers the same maximum print dimensions and automatically sets nozzle height. In an independent hands-on test, its leveling needed no manual correction. That means less calibration work for you.
The packages differ, though. The current MINI+ purchase includes an enclosure; the basic A1 mini is an open printer without one. Whether you need that enclosure depends on what you’ll print. Bambu doesn’t recommend the A1 mini for ABS, ASA, polycarbonate or nylon, so it isn’t an equivalent substitute for those materials.
For the MINI+, budget for filament, a suitable extra sheet if you’ll print PETG regularly, and the optional Wi-Fi module if Ethernet won’t work in your room. Enclosure filtration is another optional purchase. The current printer package includes the filament sensor and smooth sheet; older descriptions that treat the sensor as an extra don’t describe that bundle.
Prusa’s strongest argument is the help available when you need to understand or repair the printer. It sells individual belts, fans, sensors and filament guide tubes, publishes illustrated repair instructions and provides printable files for plastic parts. That makes it easier to find a replacement and instructions when something wears out.
Prusa also offers English chat support around the clock, including for printers outside warranty. Its standard warranty for US buyers is one year, with normal wear excluded. Support access is useful, but it doesn’t promise an immediate fix. Nor do successful review prints establish that the MINI+ will last longer or break less often than a rival.
Prusa has continued updating the software: the MINI received stable firmware 6.4.2 in June 2026, years after launch. If you already use PrusaSlicer and maintain another Prusa, that familiarity can justify paying more.
Who Should Choose The MINI+?
Choose the MINI+ as your first printer if your projects fit its small plate, you’re willing to learn first-layer adjustment and you value being able to follow a repair guide later. The enclosure strengthens its appeal when you have a specific use for it and enough room to install it properly.
As a second printer, it makes sense for small jobs that would otherwise occupy your larger printer, especially if you already work in PrusaSlicer. Check how many parts fit on its plate before counting on it for batches.
Look elsewhere if large prints or very soft flexible parts are your main goal. For a beginner making small PLA and PETG objects, the A1 mini is the easier recommendation.


