Prusament PC Blend Review
Premium engineering filament; generally more expensive than PETG.
Our verdict
I’d choose standard Prusament PC Blend for compact functional parts that need extra heat resistance, provided the printer can meet its temperature and build-surface requirements. For ordinary holders and brackets at moderate temperatures, I’d start with the cheaper, easier-printing PETG.

Best atHeat-exposed functional prototypes and mechanical parts that you can verify under their intended load.
Less suited toSimple everyday prints, large parts without an enclosure, and printers unable to sustain the required temperatures.
The Key Specs
| Printing temperatures | 265–285°C nozzle; 100–120°C bedCheck the documented hotend and bed ratings before buying. |
|---|---|
| Heat resistance | 113°C at 0.45 MPa; 93°C at 1.80 MPaThese are heat-deflection results under load, not continuous-use temperature ratings. |
| Nozzle | 0.4 mm brass recommendedStandard PC Blend does not require a hardened nozzle. |
| Larger parts | Enclosure recommendedKeeping the surrounding air warm helps reduce warping; a heat-retaining cabinet still needs ventilation. |
| Part strength | Print orientation mattersPosition the main pulling force along the layers where possible, then check the actual part under its intended load. |
| Storage / drying | Sealed storage with desiccant; 85°C for five hours if drying is neededRoutine drying is usually unnecessary; check that both dryer and spool can handle the heat. |
Which PC Blend Spool Should You Buy?
- Standard PC Blend, 900g
- I’d start here for modest-sized parts. Compare equal filament weights when shopping.
- Standard PC Blend Jet Black, 2kg
- Choose the larger spool for repeated jobs once you have verified your setup.
- Color choice
- Jet Black, Urban Grey, Natural, Prusa Orange and Prusa Pro Green are listed; choose the appearance your part needs.
Budget For Preparation And Storage. Allow for a glue-stick separation layer, sealed storage and desiccant, plus an enclosure and ventilation if your setup lacks them. If drying becomes necessary, you need a dryer capable of maintaining 85°C. Hardware upgrades can make a one-off part less economical than having it printed for you.
Also consider: Prusament PETG. Generally costs less and prints at lower temperatures with little warping; an easier starting point for everyday functional parts at moderate temperatures.
More Handling And Compatibility Details
| Reviewed grade | Standard polycarbonate blend. PC Blend Carbon Fiber is a separate, abrasive formulation with different requirements. |
|---|---|
| Build sheet | Use a glue separation layer on Prusa smooth PEI and textured sheets. Clean satin can be used without glue occasionally; glue is recommended for frequent use. Follow other sheet makers’ guidance. |
| Cooling / adhesion | Start with the PC Blend profile. The technical sheet suggests 20% fan; adjust for geometry. A brim can help hold edges down. |
| Spool heat limits | Redesigned black spools introduced in October 2025 tolerate up to 90°C. Older black cardboard-core spools need Prusa’s screw reinforcement before high-temperature drying; older grey spools tolerate up to 90°C without it. |
| Original Prusa XL | Prusa recommends drying for its idle heated tools, even when routine drying would otherwise be unnecessary. |
I’d consider Prusament PC Blend when you need a functional part that can handle heat and mechanical stress, and your printer can manage its demanding temperatures. For an ordinary room-temperature holder or bracket, I’d usually start with PETG. PC Blend’s extra heat resistance is the main reason I’d accept the added printing effort.
This review covers standard PC Blend, a polycarbonate mixture made easier to print through blending. PC Blend Carbon Fiber is a separate filament that wears nozzles down and has different requirements. Standard PC Blend works with a brass nozzle, but it still needs careful printing: a strong plastic doesn’t automatically make every printed part strong.
What Your Printer Needs For PC Blend
Prusa specifies 275 ±10°C for the nozzle (265–285°C) and 110 ±10°C for the heated bed (100–120°C). Check your printer’s documented operating limits before buying. Being able to enter a temperature on its screen isn’t enough; the hotend, which melts the filament, and bed must be rated to maintain it.
A Bowden printer, which pushes filament through a tube to the hotend, isn’t automatically unsuitable. All-metal hotends are available for Bowden systems. A plastic liner in the hot section can limit the temperature it can safely handle, so check the hotend’s construction and rating. Standard PC Blend doesn’t require a hardened nozzle; Prusa recommends 0.4mm brass.
Protect your build surface. On Prusa’s smooth PEI and textured powder-coated sheets, apply a glue-stick separation layer. Its purpose here is to let the print release without damaging the coating.
Prusa allows occasional PC Blend printing on clean satin sheets without glue, but recommends glue for frequent use to reduce wear. For another brand’s sheet, follow that maker’s material guidance.
Start with your printer’s PC Blend profile, the preset printing settings. Prusa’s technical sheet suggests 20% part-cooling fan speed, with adjustments for the shape: bridges across gaps need cooling, while larger parts without bridges may benefit from switching it off. A brim—a removable border around the first layer—can help hold the edges down.
An enclosure is a sensible priority for larger parts. Warping happens when cooling plastic shrinks and pulls corners away from the bed. Keeping the surrounding air warm reduces that shrinkage during printing.
One weekend trial reported smooth surfaces on roughly eight to ten small prints after early failures and first-layer adjustment. That’s encouraging for small jobs, but it doesn’t establish reliability for a large housing or make that adjustment a universal fix.
Plan ventilation too. Use an extraction system that captures emissions at the printer, or a properly ventilated enclosure. A cabinet that keeps heat in doesn’t necessarily keep printing emissions out of your room. You can’t judge safety by smell.
How PC Blend Handles Pulling, Bending And Impacts
Think about how your part could fail. Tensile strength describes resistance to being pulled apart, while stiffness describes how much it bends under load. Impact resistance concerns sudden blows. Layer bonding determines how readily the stacked layers of plastic separate.
In one reported test, small specimens printed flat and pulled along their layers reached about 68 MPa, versus 35 MPa for upright samples pulled across their layers. The setup was an unenclosed MK3S, brass nozzle, 275°C nozzle, 115°C bed and 20% fan. Equipment was uncalibrated, so these aren’t design ratings. MPa expresses force per unit area, not a weight your bracket can carry.
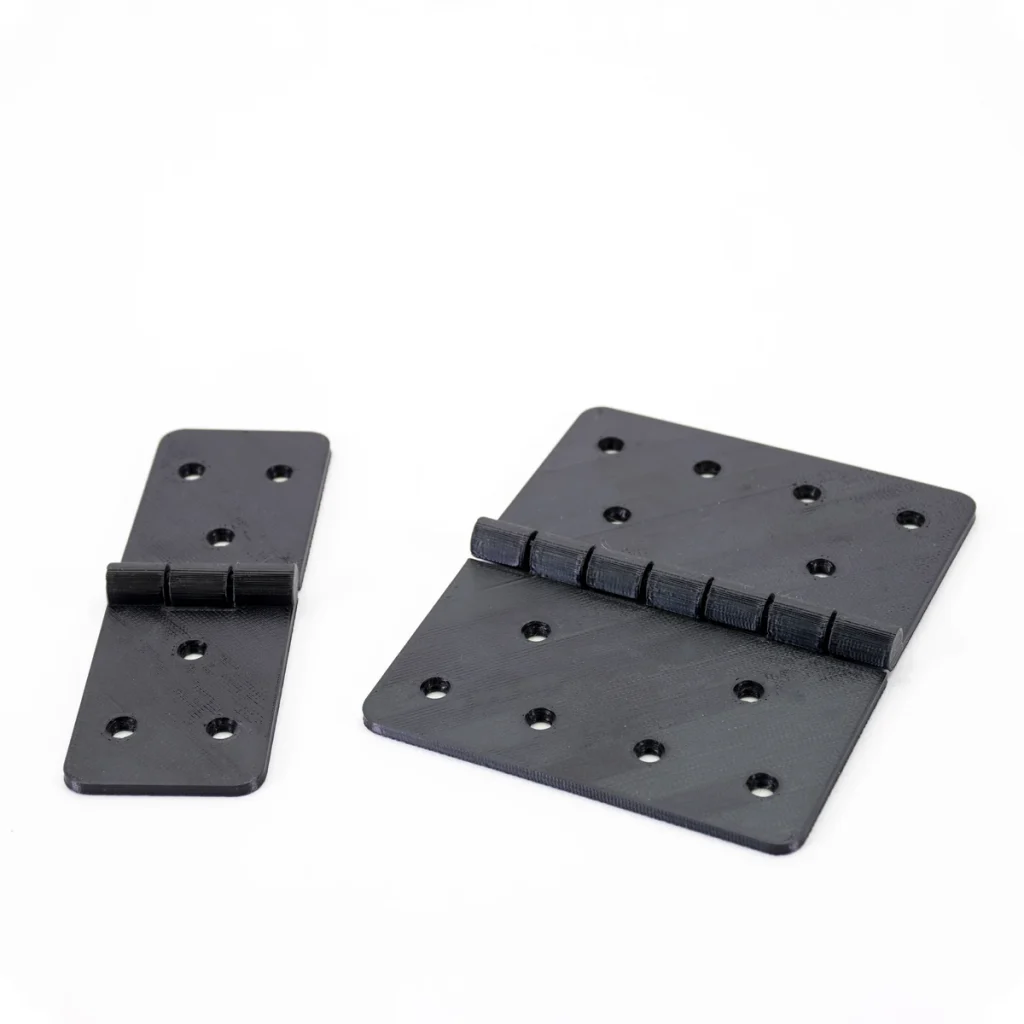
Switching from hardened steel to brass raised dried samples’ layer strength from roughly 25 to 43 MPa. It wasn’t clear whether heat transfer or the amount of plastic flowing through caused the difference. Changing nozzles also prevented a clean comparison of drying’s effect.
If you change nozzle type, check the resulting parts before trusting the previous settings. That finding doesn’t promise a similar improvement on another hotend, nor justify exceeding its temperature limits.
Later testing on a QIDI X-Max 3 used a 275°C nozzle, 0.2mm layers and solid infill, meaning the interior was filled completely. Upright PC Blend samples reached about 65% of the flat reference strength with the chamber open, 72% with its air warmed by the bed and 77% with a chamber heater set to 65°C.
Warmer air slows cooling, giving each new layer more time to bond to the one below. An enclosure helped those samples even without a chamber heater. Stay within your printer’s temperature limits.
Prusa reports a flexural modulus—a measure of stiffness in bending—of around 2.1–2.2 GPa (2,100–2,200 MPa). This isn’t a breaking-strength figure; PC Blend can still flex under load.
Its impact tests also show why shape matters: samples without a notch survived the blow, while samples with a small cut broke. “Didn’t break” in a particular test doesn’t mean your part is unbreakable.
My advice is to position the model so the main pulling force runs along its layers where possible. Also consider wall thickness: outer walls contribute substantially to strength. Filling the inside completely isn’t a substitute for choosing how the part sits on the bed. Check an actual example of your part under its intended load before relying on it.
How Much Heat Can PC Blend Parts Take?
The advertised 113°C resistance isn’t a continuous-use temperature rating. Prusa’s technical sheet identifies it as heat deflection temperature under 0.45 MPa of bending stress, using ISO 75. Under a higher stress of 1.80 MPa, the listed temperature drops to 93°C.
That distinction matters if your part must hold something while it’s hot. Heat deflection testing heats a loaded specimen until it bends by a specified amount. It doesn’t establish how long a screwed-down mount will keep its shape beside a motor, or how many heating and cooling cycles it can withstand.
A reported oven test gradually heated a bar with a load applied at its center: softening began around 110°C, with failure at 125°C. The load wasn’t sufficiently specified to equate this with ISO 75.
Don’t plan to use PC Blend at 125°C based on that result. A part can stop doing its job well before it breaks. A fan duct, for example, may become useless if it bends enough to touch a moving component.
Consider the temperature at the part, the force on it and the time it stays hot. A briefly warmed cover and a bracket supporting weight all day are different jobs.
PC Blend is a reasonable candidate for heat-exposed prototypes, but a demanding finished part needs testing under the conditions where you’ll use it. A heat-deflection number doesn’t tell you how much it will slowly change shape under constant load, called creep, or how long it will withstand repeated loading, called fatigue life.
Storing And Drying PC Blend
Prusa describes PC Blend as absorbing less moisture than conventional polycarbonate and says drying before printing isn’t normally necessary. That’s useful convenience, not moisture immunity. Keep a partly used spool in a sealed bag or box with desiccant, the moisture-absorbing packets used for dry storage.
In the MK3S test described above, drying reduced stringing—the fine threads left between printed areas—after a year of open storage. Humidity and actual dryer temperature weren’t established.
If drying is needed, Prusa now specifies 85°C for five hours for standard PC Blend. Use a dryer that can actually maintain that temperature, and check the spool before heating it. A low-temperature storage box isn’t necessarily capable of drying this material.
Prusa’s redesigned black spools, introduced in October 2025, have a plastic core with a locking mechanism. They tolerate up to 90°C without extra preparation.
Older black spools have a cardboard core and can loosen after heating above 45°C. Follow Prusa’s “Drying filament” guide to secure both sides with a screw threaded for at least 65mm; leave it fitted until the spool is empty. Older grey spools tolerate up to 90°C without a screw.
If your spool prints cleanly, routine drying usually adds little. One exception is the Original Prusa XL: Prusa recommends drying because its idle heated tools make moisture more troublesome. If stringing becomes a problem, consider drying alongside checking print settings.
Household ovens can overshoot their setting, so their displayed temperature alone isn’t enough assurance.
When PC Blend Is Worth The Extra Effort
PC Blend makes most sense when heat resistance is part of the reason you’re printing the component. A compact fan shroud or a prototype bracket near a heat source is a more convincing use than a desk organizer. You’re paying for properties the part needs, rather than choosing a demanding filament just because it sounds stronger.
PETG is the closest practical alternative for everyday functional prints. It’s generally cheaper, prints at lower temperatures and has little tendency to warp. That makes it an easier starting point for holders, cases and larger parts used at moderate temperatures. Its good layer adhesion is another reason to consider it, although that doesn’t establish that every PETG part will outperform PC Blend across layers.
Compare equal filament weights when shopping. Current standard PC Blend listings include 900g spools, while ordinary Prusament PETG commonly comes in 1kg spools. Compare the cost per kilogram, rather than the price of each reel.
Include preparation in that decision. If you already have a compatible printer, suitable sheet and enclosure, trying PC Blend is a smaller commitment. If you need hardware changes and a hotter dryer for one small replacement part, consider having that part printed for you.
I’d also make any early fit-checking prototypes in an easier material, then verify the fit again in PC Blend. Getting the screw holes and overall shape right before committing to the more demanding print can save unnecessary retries.
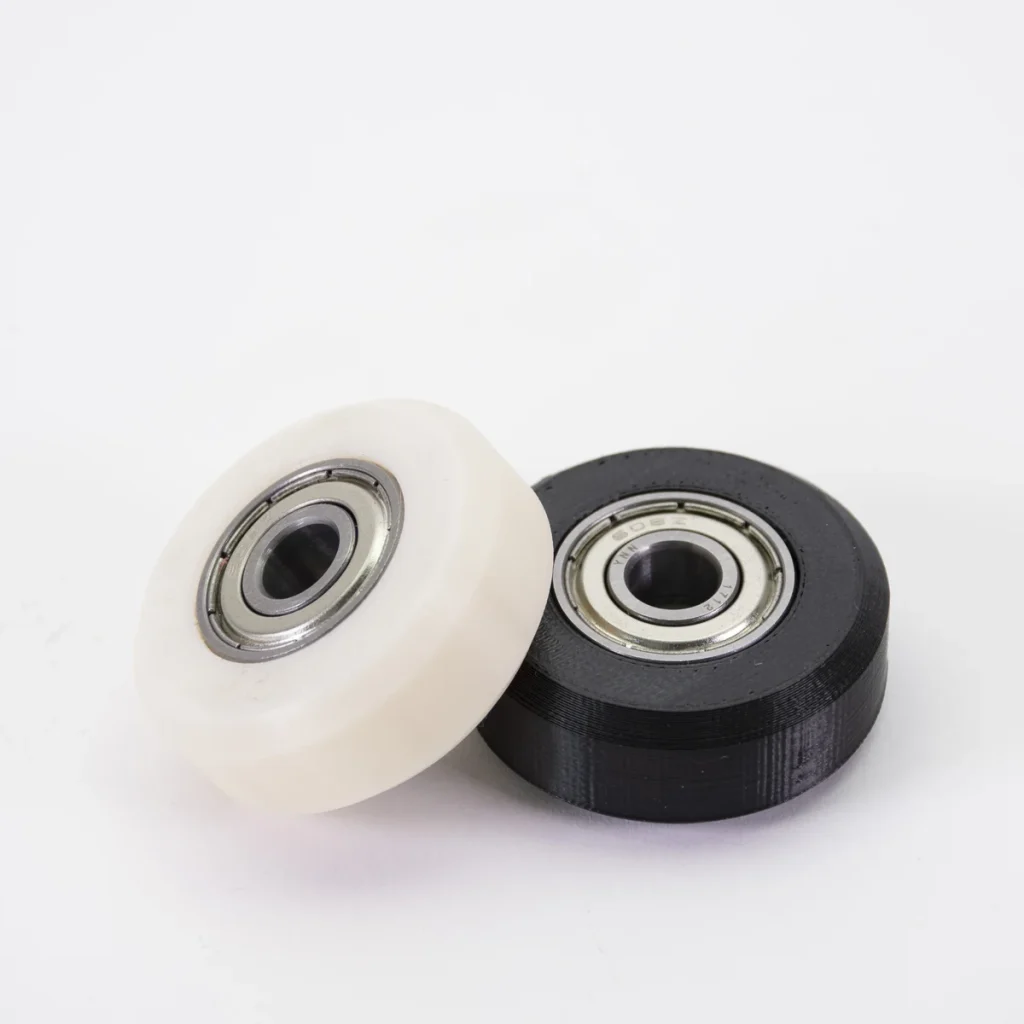
Should You Buy Prusament PC Blend?
Buy standard Prusament PC Blend if your printer can handle the temperatures and you have a functional part that needs its combination of strength and heat resistance. Start with a modest-sized part, protect the sheet and give the print orientation as much thought as the filament choice.
Prepare your printer first if it can’t meet the temperature or surface requirements. Choose PETG if your parts work at moderate temperatures and easier printing matters more than extra heat resistance. For large PC Blend prints, I’d want an enclosure before committing to a spool for that purpose.
The remaining limit is dependable service under sustained heat and load. PC Blend’s test results make it a promising material to evaluate, but they don’t supply a safe working load or lifetime for your finished part.


