UniFormation GK3 Ultra Review
Costs more than the smaller UniFormation GK3.
Our verdict
I’d choose the GK3 Ultra for recurring statues, larger prototype shells or batches that genuinely save a print run. Its capacity is the reason to buy; heating and easier handling help, but I would verify automatic refill on the exact machine before relying on it for a long job.

Best atLarge resin models and repeat batches that need more platform space.
Less suited toOccasional small miniatures, cramped workspaces or jobs that depend on unproven unattended refill.
The Key Specs
| Build volume | 300 × 160 × 300 mmA wide rectangular platform; check the model with its supports, especially front-to-back clearance. |
|---|---|
| LCD pixel size | 20 × 26 µmUseful detail potential, but pixel size is not a finished-part tolerance. |
| Heating | 25°C or 30°C settingsAllow resin to reach the temperature appropriate for its profile before printing. |
| Resin feeding | Automatic refill; manual filling supportedProve refill behavior on a small job before depending on it for a large print. |
| Platform setup | Factory aligned, with a manual leveling checkQuick-release hardware does not confirm alignment after shipping or maintenance. |
| Closed dimensions | Approximately 455 × 400 × 575 mmLeave extra room for the lid, cartridge and handling wet parts, plus washing and curing equipment. |
Budget beyond the printer. Allow for resin, cleaning supplies, suitable gloves and eye protection, ventilation, and wash-and-cure equipment large enough for your parts. Release films, filters, refill cartridges and eventual LCD replacement add ongoing costs; check replacement availability before committing to paid jobs.
Also consider: UniFormation GK3. The smaller GK3, particularly its cheaper T-screw version, retains heating and needs less bench space. Consider it if your supported models fit within 211 × 118 × 240 mm.
More Specs And Ownership Details
| Older stock / used units | Check the production label and applicable updates. UniFormation identifies a heater-related procedure mainly for 2024 machines and says 2025 production was improved. |
|---|---|
| Resin compatibility | 405 nm resin; use settings for the specific material and check them with a small calibration print. |
| Slicers / file transfer | UniFormation Slicer, CHITUBOX and Lychee; USB, Wi-Fi and Ethernet transfer. |
| Material changes | Resin remaining in the feeding lines can mix with the next material; follow the pipe-cleaning instructions. |
| Cartridge life | UniFormation limits cartridge reuse to ten times because the bottom opening can become damaged and leak. |
| Release film | UniFormation lists nFEP replacement film for the Ultra. Inspect for debris after a failed print and replace punctured film. |
| Camera monitoring | Ask the seller to demonstrate camera viewing on the exact Ultra configuration if remote monitoring is essential. |
I’d consider the UniFormation GK3 Ultra if a smaller resin printer keeps forcing you to split models into pieces or run the same batch again. Its extra space can save real work, and reported prints show fine detail and parts that fit together well. But I’d buy it for that capacity, with heating and easier handling as useful extras. Automatic refill still needs proving on your machine before you depend on it.
This is a substantial workshop purchase, including the space and equipment needed to clean and cure large prints. If you mostly want a few small miniatures, the cheaper, smaller UniFormation GK3 deserves your attention first. The Ultra earns its place when you regularly use the room it provides.
What The Ultra’s Extra Build Space Lets You Print
The GK3 Ultra’s printing limits are 300 mm across the X axis, 160 mm front to back on Y, and 300 mm tall on Z—roughly 11.8 × 6.3 × 11.8 inches. That narrow front-to-back dimension matters. You’re getting a wide rectangle, not a 300 mm square platform, so a broad statue base can run out of room sooner than its height suggests.
Reported projects include batches of GoPro handlebar mounts and Nerikson’s Heracles and the Nemean Lion sculpture. The latter was printed in separate parts, with several pieces sharing a run. That’s a useful reason to want this printer even when you don’t intend to make a huge object in one piece.
Before buying, load your actual models into a slicer, the program that prepares them for printing. Select the GK3 Ultra, turn each model to its intended printing angle, and add supports—the temporary stems that hold it while it forms. Check the space those supports occupy as well as the object itself. A bare model that barely fits may become too large once it’s ready to print.
For batches, try arranging the number of parts you actually need. Leave room to separate the supports and remove each finished piece. If your weekly order fits on one Ultra platform but takes two runs on your current printer, the benefit is concrete. If both printers can finish the order in one run, a larger platform may save you nothing.
More space also doesn’t remove the need for careful preparation. In one recent reported attempt, a large CD rack detached from its supports. A model can fit inside the printer and still be difficult to print successfully.
What The GK3 Ultra’s Prints Show About Detail And Fit
The most useful batch result is five runs of GoPro handlebar mounts in ABS-like resin, reportedly completed without missing prints. After each run, the tester used a vat-cleaning exposure: light hardens a thin sheet of resin at the bottom of the resin tank, or vat, so it can be removed with debris trapped in it.
The multipart sculpture’s joints also reportedly fitted together easily. Those results are encouraging for models and trial assemblies, but they don’t establish a production success rate or a measured dimensional tolerance.
There’s more recent support for the printer’s ability to preserve small details. An August 2026 hands-on report described a roughly 32 mm knight printed in clear-blue ABS-like resin at 0.1 mm layers. Cape and helmet details came through, although the support placement made cleanup difficult. Careful support placement and removal still matter if you want to preserve that detail.
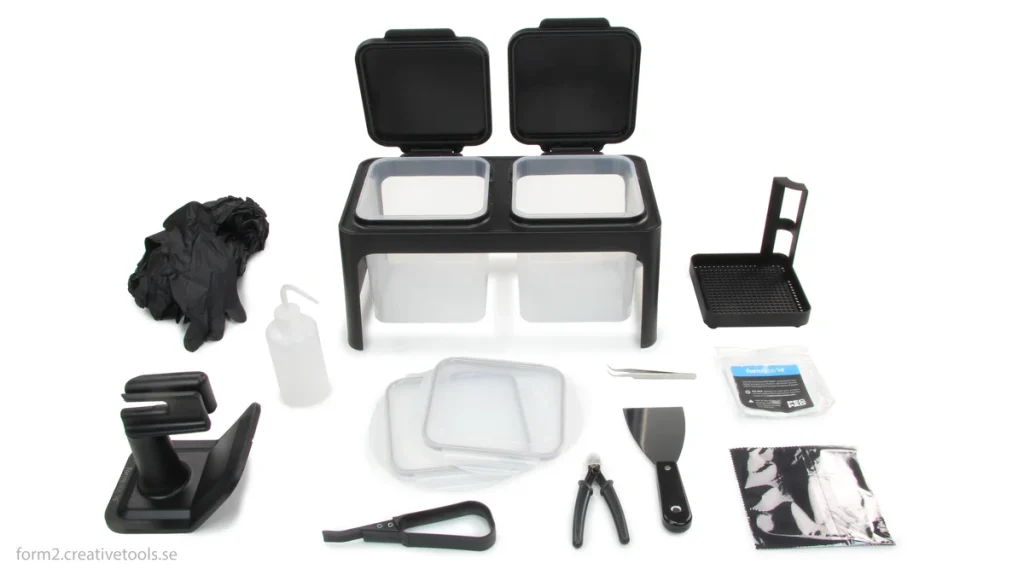
The 16K label describes the LCD screen that controls where light hardens each layer of resin. The more helpful specification is its 20 × 26 micrometer pixel size, equivalent to 0.020 × 0.026 mm across the printing surface. That’s separate from layer height, which controls the thickness of each vertical step. Neither number promises that a finished hole, peg or flat face will match its drawing to that tolerance.
For a display model, you may care most about facial features, fabric and how much sanding a joint needs. For a prototype enclosure, you need to know whether the lid closes and the screws fit. If your project depends on those dimensions, print a small section containing the important features, then wash, cure and measure it before filling the platform with copies. You’ll learn more from that than from the screen’s resolution alone.
ABS-like resin also isn’t a guarantee of the same strength or heat resistance as molded ABS plastic. Choose the material for the job, including its curing requirements, and test the finished part under the conditions you expect it to face. Successfully printing a camera mount doesn’t establish how long it will withstand vibration or sunlight.
Large jobs in the earlier report took about 15–24 hours, with some consuming more than a kilogram of resin. The report doesn’t tie every duration to a complete material and settings record. Treat those as examples of overnight-to-day-long work, not a speed rating.
Layer exposure is only part of the cycle; movement and waiting add time, and washing, support removal and curing follow afterward. There’s no matched speed test here that makes the Ultra the faster choice over another resin printer.
How Much You Can Count On The Ultra’s Automatic Refill
Refill has the potential to be especially useful on this printer. A large object or a crowded platform can use more resin than you want to pour into the vat at once. The feeding system draws from a cartridge when the level drops, reducing the need to top up during a job.
Reported experience is mixed. The earlier large-print test described successful automatic feeding, though its sample changed during testing.
In the August 2026 test with clear-blue ABS-like resin, feeding repeatedly timed out. Printing worked after automatic feeding was disabled. That tester acknowledged possible setup uncertainty, and the report doesn’t identify the firmware and production revision well enough to explain the difference.
A later account from the same tester described a deformed cartridge apparently associated with a vacuum inside it. That adds a reason to inspect the bottle and feeding behavior, but it doesn’t establish the cause of every refill complaint. These accounts support caution about depending on the feature; they don’t prove that all current units share one defect.
Follow UniFormation’s setup instructions for installing the cartridge and calibrating the feeding system before testing refill. If the calibration instructions for your unit are unclear, ask support before proceeding. I’d then start with a small print and stay available to check that resin enters the vat and stops at the intended level.
If the reading or flow is wrong, stop and resolve it with support before beginning a job that needs more resin during printing. Don’t treat a timeout as permission to keep adding resin blindly.
Use the vat’s marked maximum as the fill limit. UniFormation lists the replacement vat’s capacity as 1 kg and the refillable cartridge’s as 1,200 g. Those are mass figures, not permission to pour the same numbers of milliliters: volume depends on the resin’s density.
When checking a slicer’s estimate, include supports and compare matching units. You also need resin left in the vat for the last layers, rather than budgeting every drop into the model.
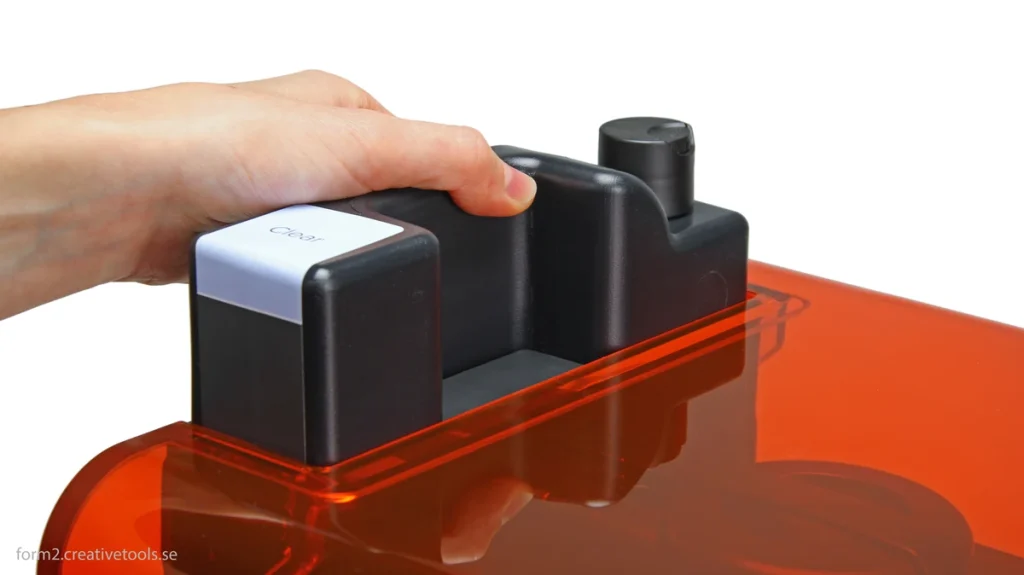
Manual filling is supported, so refill trouble doesn’t automatically make the printer unusable. It does change the buying decision if your planned jobs can’t finish with the available resin and you can’t check on them.
Changing materials adds another chore. Resin left in the feeding lines can mix with the new material even after you empty the vat, so a change from dark resin to clear resin deserves particular care. The system has a pipe-cleaning function; follow the cleaning instructions for your unit and confirm the procedure with support if they’re unclear.
UniFormation also limits cartridge reuse to ten times because the bottom opening can become damaged and leak. Check replacement availability. If you switch materials often, manual filling may suit you better than repeatedly cleaning the cartridge and lines.
Getting The GK3 Ultra Ready For Your Resin And Computer
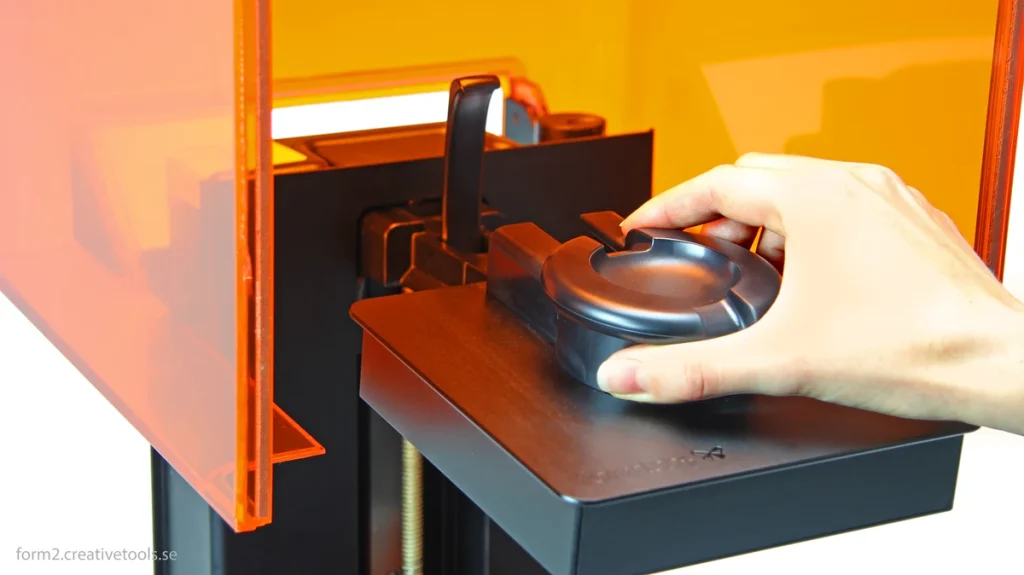
The Ultra’s build platform—the plate the print hangs from—comes aligned at the factory, but the printer doesn’t automatically level it. Follow the Ultra’s leveling-check instructions after shipping or maintenance to see whether it needs adjustment. The quick-release platform and vat simplify installation; they don’t confirm alignment. Begin with a small test before committing to a full batch.
Heating is useful when your workspace is cool. The advertised temperature choices are 25°C and 30°C, or 77°F and 86°F. Descriptions often call this chamber heating, but don’t assume a heater immersed in the resin: hands-on descriptions place the heater below the screen. Let the resin reach a suitable temperature for its profile rather than assuming the warmer setting is always better.
Production history matters here. UniFormation identifies a heater-related layer-line procedure mainly for machines made in 2024, and says 2025 production was improved. The procedure combines a hardware change with a firmware update, which changes the printer’s built-in software.
If you’re buying older stock or a used printer, check the production label and ask which changes apply. Don’t carry out an old modification on a newer machine merely because the model name matches.
The Ultra uses a 405 nm light source, so choose resin intended for that wavelength. It supports UniFormation Slicer, CHITUBOX and Lychee. UniFormation provides Windows and macOS downloads; CHITUBOX also explicitly lists the Ultra and its CTB print-file format. Check that your chosen slicer runs on your computer before ordering, and select the exact printer profile.
A material profile supplies starting settings for a particular resin and layer height. For example, Liqcreate publishes an Ultra profile for Stone Coal Black at 0.1 mm layers. That doesn’t validate its entire resin range, nor does it supply settings for an unrelated ABS-like material. Start with settings for your chosen resin and check them with a small calibration print before filling the platform.
USB, Wi-Fi and Ethernet are available for transferring files. The Ultra’s support page lists firmware 1.2.9 with SMB folder sharing and ChituManager support. SMB lets you copy a prepared file into a shared network folder. Keep USB available if network setup gets in the way.
File transfer, app status, remote controls and camera viewing are separate features. The product listing mentions an app, but the Ultra-specific documentation doesn’t clearly establish every remote function or an integrated camera workflow. Don’t assume the smaller GK3’s camera features carry over. If seeing prints from another room is essential, make a demonstration on the exact Ultra configuration a buying condition.
Making Room For The GK3 Ultra And Keeping It Running
The closed printer measures approximately 455 × 400 × 575 mm, or 17.9 × 15.7 × 22.6 inches. Published weight descriptions differ, putting it around 30–35 kg—roughly 66–77 pounds. Plan a permanent position on a sturdy bench and get help moving it. A shelf that merely fits the base isn’t enough.
You need additional room for the hinged lid, cables and top-mounted resin cartridge. One reported rack installation needed at least 85 cm between shelves to insert the bottle. Use that as a planning clue, not a guaranteed clearance specification. Confirm the open-lid and cartridge-removal space before putting the printer under a shelf.
Then plan where a wet platform or full vat will go. Quick-release catches reduce fiddling with screws, and the drip hanger lets excess resin drain back. You still need a clear, protected surface beside the machine and a short route to the wash container. Handling a large resin-covered part becomes much harder if you have to carry it across the room.
Washing removes uncured surface resin; curing uses additional light to finish hardening the cleaned print. Both need equipment that fits your largest part. Printer capacity can outgrow equipment you already own.
UniFormation offers the Cure3 Ultra for this printer, but its product text gives a two-dimension capacity figure that doesn’t clearly establish every fitting orientation. Check the usable chamber dimensions rather than assuming any 300 mm-tall print fits upright. Likewise, verify the inside of your wash basket, including space occupied by supports or a platform.
The built-in carbon filter is intended to reduce odor. That doesn’t establish safe air throughout your workspace, particularly while the cover is open or you’re washing parts. Use a separate, suitably ventilated work area, with extraction arranged to control emissions from printing and cleanup.
Keep wash containers closed when possible. Wear eye protection and gloves selected for both the resin and cleaning solvent, following their safety data sheets. If your only available space is an occupied desk without suitable ventilation, this printer isn’t a good fit.
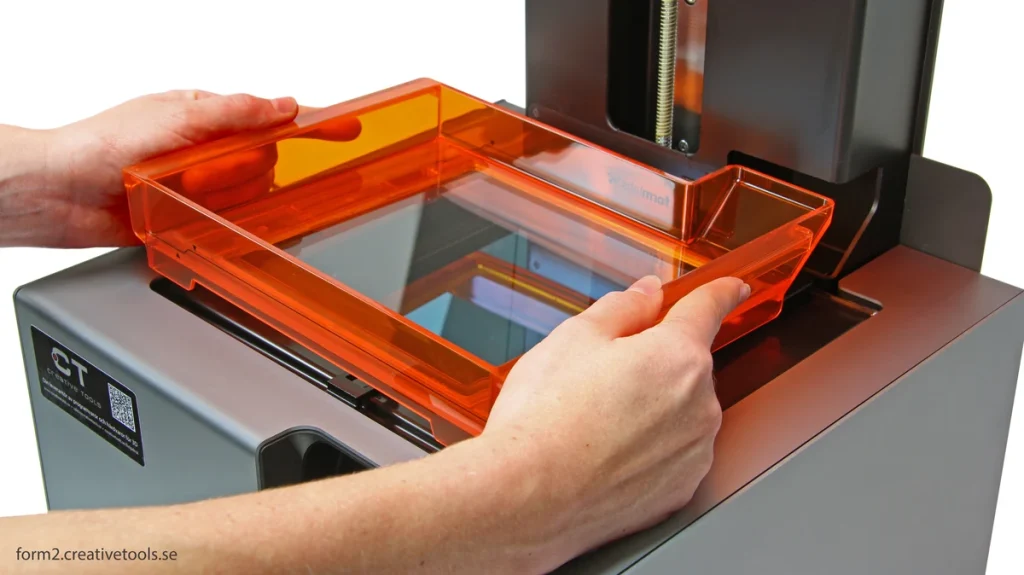
The transparent release film forms the bottom of the vat and lets each hardened layer peel away as the print rises. It’s a replaceable part: UniFormation lists nFEP film for the Ultra, while some early test machines used a different film called ACF. Their wear experience isn’t automatically transferable.
One reported test suffered a puncture after fallen support debris remained in the vat. Hard resin debris can pierce the film and let liquid resin leak onto the screen below. Inspect after failures and remove debris before printing again; replace a punctured film.
Film replacement involves multiple screws and careful installation. A spare vat can reduce downtime while you service the other one. The manufacturer lists replacement vats, films, protectors and LCDs, but a listing isn’t a promise of immediate shipment. Check parts availability before accepting workshop jobs with tight deadlines.
UniFormation advertises a one-year machine warranty. Its policy excludes ordinary consumable wear and makes you responsible for shipping a covered repair to the service center after the first three months. It also identifies faults caused by non-certified consumables as a possible paid-repair case.
Confirm coverage for your intended materials and the service arrangements before purchase; shipping a machine this heavy can matter almost as much as the replacement part.
When The GK3 Ultra Makes Sense For You
I’d consider the Ultra for recurring statue work, larger prototype shells or batches that clearly need more platform space. Bring three or four typical projects into the slicer and count the runs they require. The strongest case is a repeated saving in printing and assembly work that you’ll actually use, with enough washing and curing capacity to keep up.
If those projects fit comfortably inside 211 × 118 × 240 mm, compare the smaller UniFormation GK3, particularly the cheaper T-screw version. It retains heating and uses less bench space. Its smaller capacity is the relevant compromise here; the shared 16K label doesn’t make the two printers interchangeable. There isn’t enough controlled comparative testing to promise that either gives you better finished parts for every application.
Budget for resin, cleaning supplies, release films, filters and eventual screen replacement alongside the machine. Resin left in a clean vat isn’t automatically wasted, but supports, failures and material changes all affect what each usable part costs.
If your decision depends on unattended refill or camera monitoring, ask the seller to demonstrate those functions on the exact Ultra configuration you would buy. For jobs you plan to sell, check parts availability and service costs too: extra printing capacity is useful only while you can keep the printer running.


